 0
 EN
 English
 عربى
 Español
 русский
If you need any help, please feel free to contact us
Home / Author / Ren Xiaotong — Technical Sales Engineer for Gas Flow Meters / Industrial Vortex Flow Measurement for Steam, Gas, and Liquid Process Systems
Industrial Vortex Flow Measurement for Steam, Gas, and Liquid Process Systems
Introduction
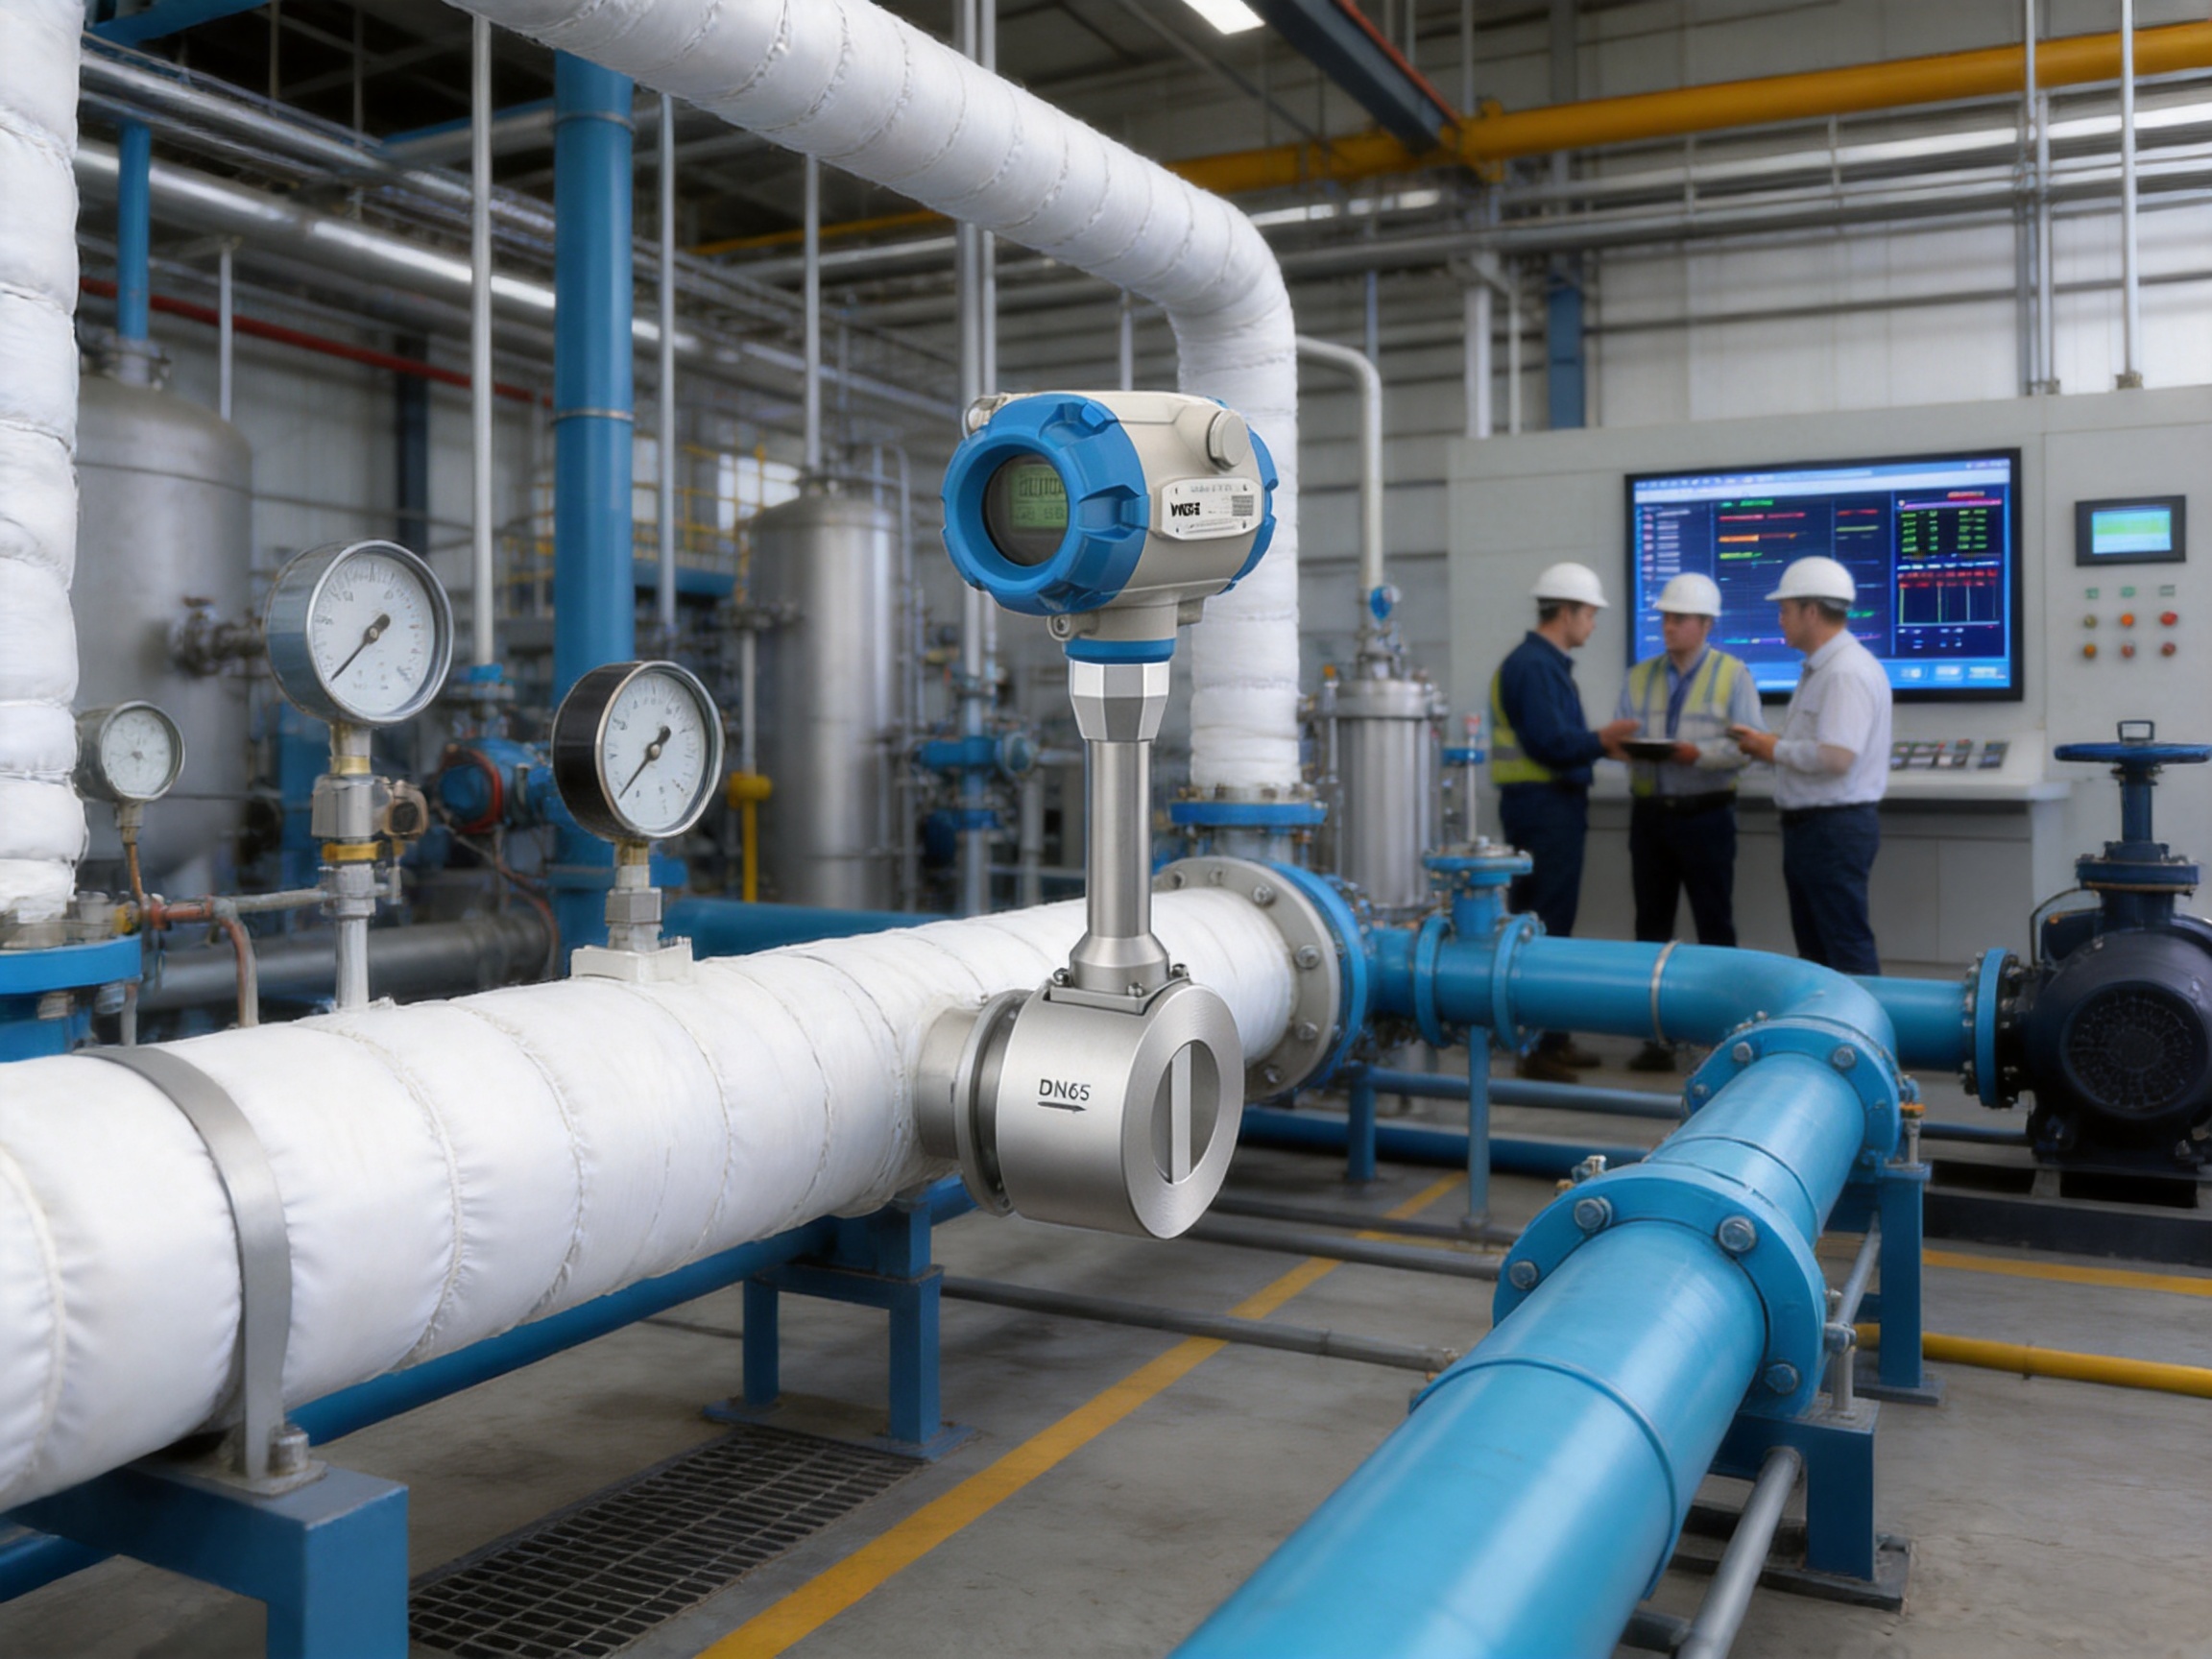
Reliable flow measurement is essential wherever industrial facilities need to control energy consumption, balance production, protect equipment, or maintain consistent product quality. Steam networks, compressed-gas systems, fuel lines, chilled-water loops, chemical processes, and utility pipelines all depend on instruments that can provide stable measurements under changing operating conditions. The MA80T Series Vortex Flowmeter is designed for these demanding duties, offering a practical measurement solution for steam, gases, and liquids in industrial process environments.
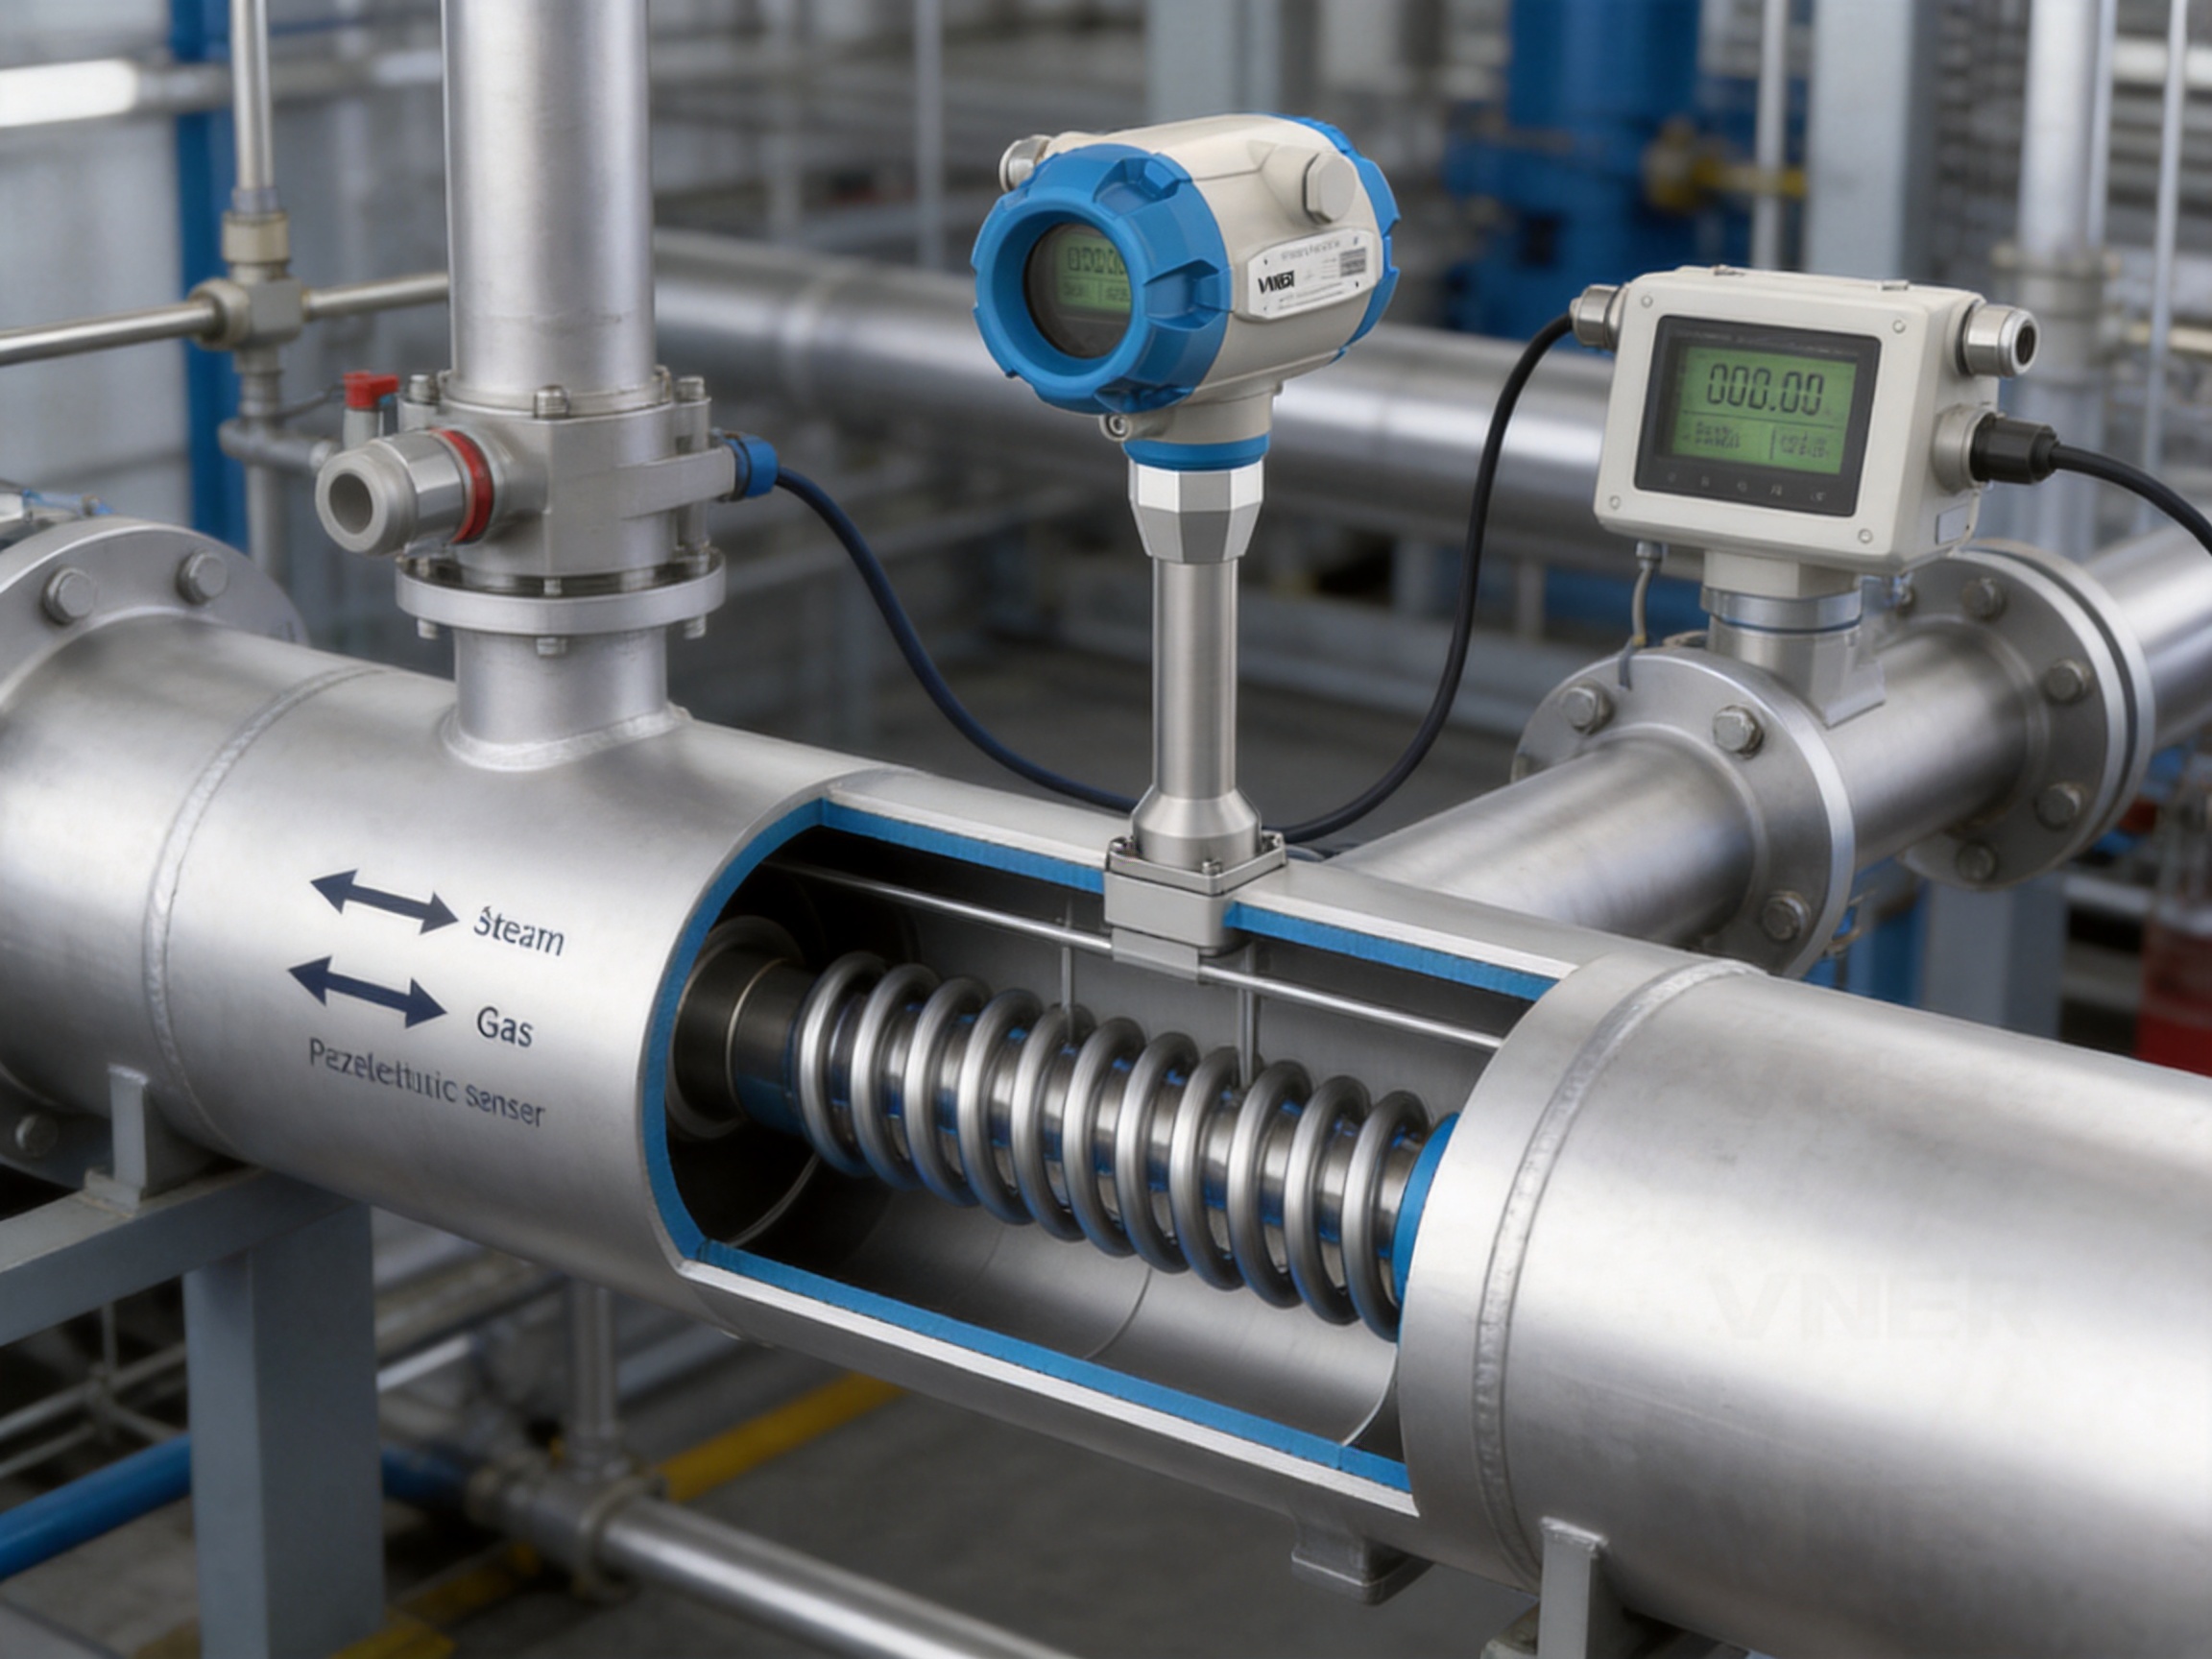
The instrument operates according to the Kármán vortex street principle. When a flowing medium passes a specially shaped bluff body, commonly known as a shedder bar, alternating vortices are generated downstream. The frequency of these vortices is proportional to the velocity of the medium. A piezoelectric sensor detects the pressure or force fluctuations associated with vortex formation, and the transmitter converts the measured frequency into a flow-rate signal.
This measurement method provides a useful balance between mechanical simplicity, process adaptability, and long-term operating stability. Unlike positive-displacement meters and other designs that rely on continuously moving internal components, the MA80T has no rotating impeller or sliding mechanical assembly inside the flow body. This reduces wear-related concerns and supports dependable operation in utility and process applications.
For industrial users, selecting a vortex flowmeter is not simply a matter of choosing a nominal pipe size. The instrument must be correctly matched to the medium, pressure, temperature, velocity range, piping arrangement, required output, and installation environment. The MA80T Series has been developed as part of a broader industrial flow measurement portfolio, with engineering, calibration, manufacturing, and application support intended to help users obtain consistent results from system design through long-term operation.
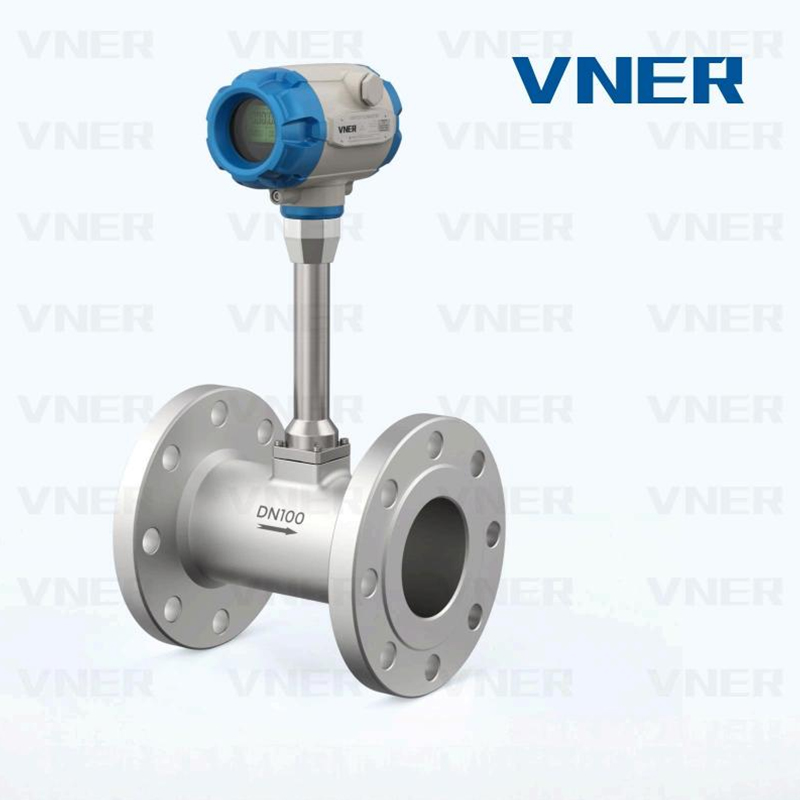
MA80T Series Vortex Flowmeter-副本
How the MA80T Vortex Flowmeter Works
The operating principle of a vortex flowmeter is based on a physical phenomenon that occurs when a fluid flows around a bluff body. At sufficiently stable flow conditions, vortices separate alternately from opposite sides of the shedder bar. This creates a repeating pattern of pressure fluctuations downstream of the obstruction. The number of vortices formed during a given period is directly related to the velocity of the fluid.
The relationship between vortex frequency and flow velocity is commonly expressed through the Strouhal relationship. In practical terms, the sensor measures the frequency of vortex shedding, while the transmitter uses programmed meter characteristics to calculate volumetric flow. With suitable compensation inputs, the system can also provide corrected volume, mass-flow-related values, or energy-management information for selected applications.
The piezoelectric sensing element is particularly suitable for vortex measurement because it can detect the periodic signal without requiring a moving mechanical pickup. Piezoelectric technology can also provide a compact sensing arrangement and good resistance to industrial vibration when the meter is correctly installed and configured.
Because vortex shedding depends on fluid velocity, the instrument is best applied within an appropriate Reynolds-number range and operating velocity window. Very low flow may not generate a sufficiently strong and stable vortex signal, while excessive velocity can increase pressure loss, noise, vibration, or erosion risk. Correct sizing is therefore a central part of successful application engineering.
The MA80T flow body is designed to maintain a defined internal geometry around the shedder bar and sensing region. The stability of this geometry is important because even small dimensional changes can influence the relationship between vortex frequency and flow rate. Manufacturing consistency, dimensional control, calibration, and traceability are consequently important contributors to measurement performance.
Measurement of Steam, Gas, and Liquid
Vortex technology is widely used for steam and gas measurement because these media often have relatively stable flow characteristics and require instruments with a broad operating range. Saturated steam, superheated steam, compressed air, natural gas, nitrogen, oxygen, carbon dioxide, and fuel gas can all be considered for vortex measurement when pressure, temperature, cleanliness, and velocity conditions are suitable.
Liquid measurement is also possible for clean, relatively low-viscosity liquids. Typical examples include water, hot water, chilled water, condensate, and selected process liquids. The liquid should remain sufficiently stable and free from excessive entrained gas. Large quantities of bubbles, flashing, solids, or severe pulsation may affect signal quality and should be evaluated during meter selection.
The MA80T is therefore a versatile option for facilities that need one general measurement technology across several utility systems. Standardization can simplify training, spare-parts planning, commissioning procedures, and maintenance documentation, particularly when a plant measures steam, water, and gas in different areas.
Core Advantages of the MA80T Series
No Moving Parts in the Main Measuring Principle
One of the most important advantages of vortex measurement is the absence of an internal rotating mechanism. Turbine flowmeters, for example, use a rotor that turns as the fluid passes through the meter. Positive-displacement meters use chambers, gears, lobes, or other moving components. These designs can be highly effective in suitable applications, but their moving parts may be subject to wear, contamination, bearing damage, or changes in performance over time.
The MA80T uses a fixed bluff body and a piezoelectric sensor instead of a rotating mechanical element. This reduces the number of wear-sensitive components inside the flow path. It can also reduce the need for routine mechanical servicing in applications where the process medium is clean and the meter is properly sized.
The absence of moving parts does not mean that installation and inspection can be ignored. Process vibration, improper support, severe pulsation, condensation, corrosion, and incorrect flow velocity can still affect performance. However, the basic construction provides a strong foundation for stable measurement and simplified maintenance compared with certain mechanical meter technologies.
Wide Process Applicability
The MA80T can measure steam, gas, and liquid, allowing it to serve a wide range of industrial functions. This flexibility is valuable in facilities where process engineers need to monitor several utilities with different physical properties. A single vortex platform can be used for boiler steam, compressed air, natural gas, hot water, chilled water, and condensate, subject to detailed application verification.
In oil and gas facilities, the meter may be applied to fuel gas, natural gas, burner systems, saturated steam, and condensate pipelines. In food and beverage plants, it can support clean-steam monitoring, carbon dioxide injection, and liquid utility measurement. In pharmaceutical systems, it may be used for clean steam in sterilization or purified-water-related applications when material, hygienic, and validation requirements are satisfied.
In power generation and utility plants, vortex flow measurement is often used for boiler steam, auxiliary steam, compressed air, cooling-water circuits, and heat-recovery systems. In chemical and petrochemical facilities, it can be considered for utility gas, process vapor, steam, and compatible liquids.
High-Temperature and High-Pressure Capability
Industrial systems frequently operate under conditions that exceed the capabilities of ordinary commercial flow instruments. The MA80T Series is designed for demanding environments, with product information specifying pressure capability up to 4.0 MPa and temperature capability up to 350°C for applicable configurations.
These specifications make the instrument suitable for many steam and high-temperature utility services. Nevertheless, the actual allowable pressure and temperature depend on the selected body, flange rating, sensor construction, electronics, gasket, connection, and installation conditions. Engineers should always confirm the certified rating of the specific configuration before ordering or commissioning the meter.
High-temperature measurement also requires careful consideration of transmitter location, insulation, heat dissipation, ambient temperature, and signal-cable routing. Where remote electronics are used, the installation can separate the sensing body from the display and signal-processing unit. This can help protect electronics from excessive process heat and improve access for operators.
Low Pressure Drop
Every obstruction in a pipeline creates some pressure loss. Excessive pressure loss can increase pumping or compression requirements and reduce overall system efficiency. The MA80T uses a comparatively streamlined measurement body and a defined shedder-bar arrangement to provide measurement without the large pressure losses associated with some more restrictive flow devices.
Low pressure drop is particularly important in compressed-air systems, natural-gas distribution, steam networks, and circulation loops. Even a small pressure penalty can become significant when multiplied across many operating hours. By reducing unnecessary resistance, an appropriate vortex meter can support better energy management while still providing the required flow information.
Actual pressure loss depends on nominal diameter, medium density, operating velocity, pressure, temperature, and internal design. It should therefore be reviewed during sizing rather than assumed to be identical for every application.
Flexible Installation Options
The MA80T Series supports horizontal and vertical pipeline installation when the relevant application requirements are met. Flange and wafer versions are available to adapt to different piping standards and space constraints. The choice between flange and wafer construction depends on pressure class, maintenance preferences, available face-to-face length, piping design, and local standards.
Vertical installation can be useful where floor space is limited or where the process arrangement naturally supports upward or downward flow. For liquids, the pipe should generally remain full to maintain a stable measurement condition. For steam and gas systems, the direction of flow, drainage, condensation control, and pipe support should be reviewed carefully.
Installation flexibility can reduce retrofit difficulty and help engineers integrate the instrument into existing plants. However, the meter should not be installed solely because it physically fits the pipeline. Straight-run requirements, nearby valves, reducers, elbows, pumps, compressors, control devices, and flow disturbances must be considered during design.
| Feature | MA80T Series Benefit | Typical Industrial Value |
|---|---|---|
| Measurement principle | Kármán vortex shedding with piezoelectric detection | Stable frequency-based measurement for steam, gases, and liquids |
| Mechanical construction | No rotating measuring element | Reduced wear-related maintenance and good long-term repeatability |
| Temperature capability | Applicable configurations up to 350°C | Suitable for many high-temperature steam and process duties |
| Pressure capability | Applicable configurations up to 4.0 MPa | Useful in industrial steam and gas distribution networks |
| Connection options | Flange and wafer versions | Adaptation to new installations and retrofit projects |
| Installation direction | Horizontal or vertical installation | Greater flexibility in plant layout and piping design |
| Primary applications | Steam, gas, water, condensate, and selected process liquids | One platform for multiple utility and process measurement duties |
| Signal processing | Frequency detection with transmitter calculation | Real-time flow indication and integration with control systems |
Comparison with Other Flowmeter Technologies
Vortex Compared with Turbine Flowmeters
Turbine flowmeters measure flow through the rotational speed of an internal rotor. They can provide good performance in clean liquids and gases, especially when the flow range and viscosity are well controlled. However, the rotor, bearings, and shaft are mechanical components that may experience wear or become affected by contamination.
The MA80T eliminates the rotating rotor from the measuring principle. This can be advantageous in steam, utility gas, and general industrial services where long-term simplicity is more important than extremely low-flow mechanical response. The vortex meter may also reduce concerns related to bearing replacement and rotor fouling.
On the other hand, a turbine meter may remain preferable for certain clean-liquid duties or applications requiring a particular low-flow response. The correct comparison must be based on actual process conditions rather than a general assumption that one technology is always superior.
Vortex Compared with Electromagnetic Flowmeters
Electromagnetic flowmeters are highly effective for conductive liquids and are widely used in water, wastewater, slurry, and chemical applications. They have no obstruction in the same sense as a vortex shedder bar and can offer excellent performance in many liquid services.
Electromagnetic meters cannot normally measure non-conductive liquids, steam, or most gases. A vortex flowmeter offers a broader medium range because it relies on fluid velocity and vortex formation rather than electrical conductivity. This makes the MA80T more suitable when one facility needs to measure both steam and gas as well as water or selected liquids.
For highly conductive liquids containing solids or abrasive particles, an electromagnetic meter may be the better solution. For steam and gas networks, vortex technology often provides a more direct and practical choice.
Vortex Compared with Coriolis Mass Flowmeters
Coriolis flowmeters measure mass flow directly by analyzing the motion of vibrating tubes. They can provide highly accurate mass-flow measurement and may also report density and temperature. Their capabilities are valuable for custody transfer, batching, blending, and high-value process materials.
The MA80T is generally simpler and more economical for large utility lines, steam distribution, compressed air, and general gas measurement. Large Coriolis meters can be expensive, heavy, and sensitive to installation conditions. A vortex meter can provide an efficient alternative where volumetric flow or compensated utility flow is sufficient.
When the process requires direct high-accuracy mass measurement, density information, or precise low-flow batching, Coriolis technology may have clear advantages. When the priority is robust utility monitoring over a broad line-size range, vortex measurement can offer a more practical balance.
Vortex Compared with Differential-Pressure Meters
Orifice plates, venturi tubes, flow nozzles, and other differential-pressure devices are proven technologies used across the process industries. They calculate flow from the pressure difference generated by a restriction. Their principal benefits include familiarity, established standards, and applicability to many fluids.
However, differential-pressure measurement requires pressure taps, impulse lines, and transmitters. Impulse lines can be affected by blockage, condensation, freezing, leakage, or incorrect installation. The permanent pressure loss can also be significant, especially with restrictive primary elements.
The MA80T integrates the flow-sensing body and frequency-based detection into one instrument. This can simplify installation and reduce the number of external components. It may also provide a lower pressure-loss option for selected systems. Differential-pressure meters remain highly useful where standardized calculations, very large line sizes, or specific process conditions make them preferable.
Vortex Compared with Ultrasonic Flowmeters
Ultrasonic flowmeters determine flow velocity using the transmission or travel-time difference of ultrasonic signals. Clamp-on versions can be installed without cutting the pipe, while inline versions can provide highly capable measurement for liquids and gases.
Ultrasonic instruments can be attractive for temporary surveys, large pipelines, clean liquids, and applications where minimal obstruction is required. Their performance may depend strongly on pipe condition, acoustic properties, installation geometry, and the presence of bubbles or solids.
The MA80T provides an inline, industrially standardized measurement body with a clear physical relationship between vortex frequency and flow velocity. It can be easier to specify for permanent steam and gas installations where the pipeline is being designed or modified for a dedicated meter.
Applications Across Industrial Sectors
Oil and Gas
Oil and gas facilities use flowmeters for fuel gas, natural gas, steam, condensate, compressed air, nitrogen, and utility systems. The MA80T can support monitoring of gas consumption at boilers, furnaces, heaters, burner trains, and plant distribution headers when the pressure, temperature, composition, and velocity range are suitable.
Accurate fuel-gas measurement helps operators compare consumption between production units, identify abnormal demand, and optimize combustion. Steam and condensate measurement can support heat-balance calculations and reveal losses caused by failed traps, insulation problems, or inefficient equipment.
In these environments, material compatibility, hazardous-area classification, grounding, signal integrity, and safety procedures must be addressed. Product configuration should be matched to the required electrical approvals and site standards.
Power Generation
Power plants depend on steam and water measurement at many points, including boilers, turbines, heat-recovery systems, auxiliary systems, deaerators, and district-heating circuits. The MA80T can assist with steam-flow monitoring and utility allocation where its pressure, temperature, and accuracy characteristics meet the project requirements.
Steam measurement is useful for evaluating boiler performance, balancing turbine inputs, monitoring heat-recovery systems, and comparing output against fuel consumption. Water measurement in cooling or heating loops can support thermal-energy calculations and help identify abnormal circulation conditions.
High-temperature service places additional demands on installation. Adequate straight pipe, proper insulation practices, thermal expansion management, and suitable electronics protection can improve reliability and reduce measurement disturbances.
Food and Beverage Processing
Food and beverage plants consume steam, hot water, chilled water, compressed air, carbon dioxide, nitrogen, and cleaning fluids. Flow monitoring can support pasteurization, sterilization, carbon dioxide injection, process heating, cleaning-in-place systems, and utility cost allocation.
For hygienic or clean-service applications, the wetted materials, surface finish, connection design, cleaning procedure, and regulatory requirements must be verified. The MA80T may be considered for clean steam or compatible liquid duties when the selected construction meets the plant’s hygienic and validation requirements.
Measurement data can also contribute to sustainability programs. By monitoring steam and hot-water consumption at individual production lines, operators can identify energy-intensive operations and compare actual usage with production volumes.
Pharmaceutical Manufacturing
Pharmaceutical facilities require careful control of clean utilities and process conditions. Clean steam used for sterilization-in-place and autoclave systems must be monitored in a way that supports process repeatability and documented validation procedures. Purified-water and water-for-injection systems require hygienic design and strict material controls.
In pharmaceutical service, the flowmeter is only one part of the compliance system. Users must also evaluate sensor materials, surface finish, dead legs, drainability, cleaning and sterilization conditions, calibration records, installation orientation, and data integrity. A suitable MA80T configuration can provide real-time monitoring where the application requirements and validation framework are satisfied.
Chemical and Petrochemical Processing
Chemical plants handle a wide range of gases, vapors, solvents, water-based liquids, steam, and utility media. The MA80T can be applied to compatible process streams and utility networks, including heating steam, inert gas, instrument air, reaction-media services, and cooling-water systems.
Material compatibility is essential. Engineers should consider corrosion, chemical concentration, temperature, pressure, erosion, deposits, and possible reactions with wetted components. For corrosive vapors or aggressive liquids, the selected body and sensor materials should be checked against the complete process composition rather than only the product name.
Reliable flow information can improve dosing, process control, energy allocation, and troubleshooting. In large plants, standardizing measurement technology across utility services may also reduce the complexity of maintenance and spare-parts management.
HVAC and Building Automation
District heating, district cooling, commercial buildings, campuses, and industrial facilities all depend on stable circulation of hot water and chilled water. Vortex flowmeters can be used in suitable water-loop conditions to monitor flow and support thermal-balance calculations.
When paired with temperature sensors, flow data can help calculate heating or cooling energy. Operators can use this information to assess pump performance, detect blocked strainers, balance branches, and improve building-control strategies.
For HVAC systems, the meter should be sized to the actual minimum and maximum flow rather than only the nominal pipe size. Oversizing can reduce measurement sensitivity at low demand, while undersizing may cause excessive velocity and pressure loss.
Textile, Dyeing, and Pulp and Paper
Textile and dyeing plants consume process steam, hot water, compressed air, and dye liquor. Flow measurement helps regulate heating, control batching, improve repeatability, and identify utility losses. Pulp and paper facilities use steam, condensate, white liquor, black liquor, process water, and other streams that require careful evaluation of viscosity, solids content, and chemical compatibility.
The MA80T is especially suitable for clean or relatively stable steam, gas, and liquid services. Streams containing significant solids, fiber, entrained air, or high viscosity may require another meter technology or a detailed application review. Selecting the correct instrument for each individual process line is more important than applying one meter type universally.
Steam Measurement and Thermal-Energy Management
Steam is one of the most important industrial energy carriers. It transfers heat efficiently, but its generation and distribution can represent a major operating cost. Measuring steam flow at boilers, headers, production lines, and end users allows companies to understand where energy is produced, consumed, and lost.
The MA80T can be used for saturated-steam or superheated-steam applications within the relevant operating range. Pressure and temperature information may be used for compensation so that changing steam conditions do not produce misleading flow comparisons. Depending on the transmitter and system architecture, compensated data can support mass-flow estimation, thermal-energy balancing, or cost allocation.
In a steam network, pressure and temperature are rarely constant. Demand changes when production equipment starts or stops, when weather conditions vary, or when different shifts operate at different capacities. A flowmeter that reports only uncorrected volumetric flow may not provide enough information for energy accounting. Engineers should determine whether the project requires actual volume, standard volume, mass flow, or energy flow and specify the relevant inputs accordingly.
Steam measurement also helps identify equipment problems. A sudden increase in condensate or steam consumption may indicate a failed steam trap, leaking valve, damaged insulation, control instability, or process heat-transfer issue. Trend data from the flowmeter can therefore support preventive maintenance and energy-efficiency programs.
Gas Flow Optimization
Gas measurement is important for combustion control, production accounting, compressed-air management, inerting, and process safety. The MA80T can be considered for natural gas, fuel gas, air, nitrogen, carbon dioxide, and other compatible gases when the flow conditions fall within the meter’s operating range.
In combustion systems, fuel-gas data can be compared with air-flow information to improve the fuel-air ratio. Better ratio control may improve thermal efficiency, reduce incomplete combustion, and lower emissions. Stable gas measurement can also help operators detect burner imbalance, regulator problems, leakage, or unexpected demand.
Compressed-air systems are another important application. Compressed air is often one of the most expensive utilities in a plant because energy is consumed continuously to maintain pressure. Flow measurement at the compressor room, major distribution headers, and production areas can reveal leakage and demand peaks.
For gas measurement, pressure and temperature compensation may be required because gas density changes significantly with operating conditions. The meter selection should include gas composition, molecular weight, compressibility, operating pressure, temperature, minimum flow, maximum flow, and required reference conditions.
Engineering and Sizing Considerations
Flow Range
The flowmeter should be selected according to the actual operating range, including minimum, normal, and maximum flow. A meter sized only by line diameter may perform poorly if the normal flow is too low to generate a strong vortex signal. Conversely, excessive flow may produce unnecessary pressure loss, vibration, or erosion.
Engineers should also consider startup, shutdown, seasonal variation, production changes, and emergency operating conditions. A process that usually operates at a stable flow may experience brief but significant peaks. These conditions should be compared with the meter’s allowable range and output capabilities.
Pipe Size and Line Reduction
In some applications, the meter size is smaller than the process line and reducers or expanders are used. This can be acceptable when the resulting velocity, pressure loss, and flow profile remain suitable. The transition should be designed to avoid excessive turbulence or asymmetrical flow entering the meter.
For large pipelines with low velocity, reducing the line around the flowmeter can improve measurement sensitivity. However, the reduction must be evaluated carefully for steam quality, gas pressure loss, liquid cavitation risk, and maintenance access.
Straight Pipe Requirements
Vortex meters perform best when the flow entering the meter is sufficiently developed and free from strong swirl. Elbows, tees, valves, pumps, compressors, control valves, reducers, and expanders can disturb the flow profile. Adequate straight pipe upstream and downstream helps the meter operate within its intended conditions.
The required length depends on the type and position of the upstream disturbance. The installation manual and project engineering standard should be followed. A flow conditioner may be considered when space is limited, but it should not be used as a substitute for proper application review.
Liquid Pipeline Conditions
For liquid applications, the pipeline should remain full. Downstream pressure must be sufficient to prevent flashing or cavitation, particularly with hot liquids. The meter should not be installed at a high point where air can accumulate or in a location where the line may drain during normal operation.
Entrained gas can produce unstable readings because the meter is measuring a mixture rather than a uniform liquid. If air or gas entrainment is unavoidable, a different technology or additional conditioning may be required.
Steam and Gas Condensation
Steam and gas installations require attention to condensation. Water accumulation in steam lines can cause inaccurate measurement, water hammer, corrosion, or mechanical damage. Proper drainage, slope, separators, insulation, and trap arrangements should be provided according to the process design.
Gas lines may also experience condensation when temperature falls below the dew point. The installation should prevent liquid pockets from forming around the meter and should maintain process conditions that are consistent with the selected application.
Vibration and Mechanical Support
Although the piezoelectric sensing principle is designed for industrial service, excessive external vibration can interfere with the measured signal. Nearby reciprocating machinery, compressors, pumps, unsupported piping, or structural resonance should be evaluated.
Pipe supports should be strong enough to prevent movement, but they should not impose excessive mechanical stress on the flowmeter body. Thermal expansion should also be accommodated, especially in high-temperature steam lines.
Manufacturing Strengths and Quality Control
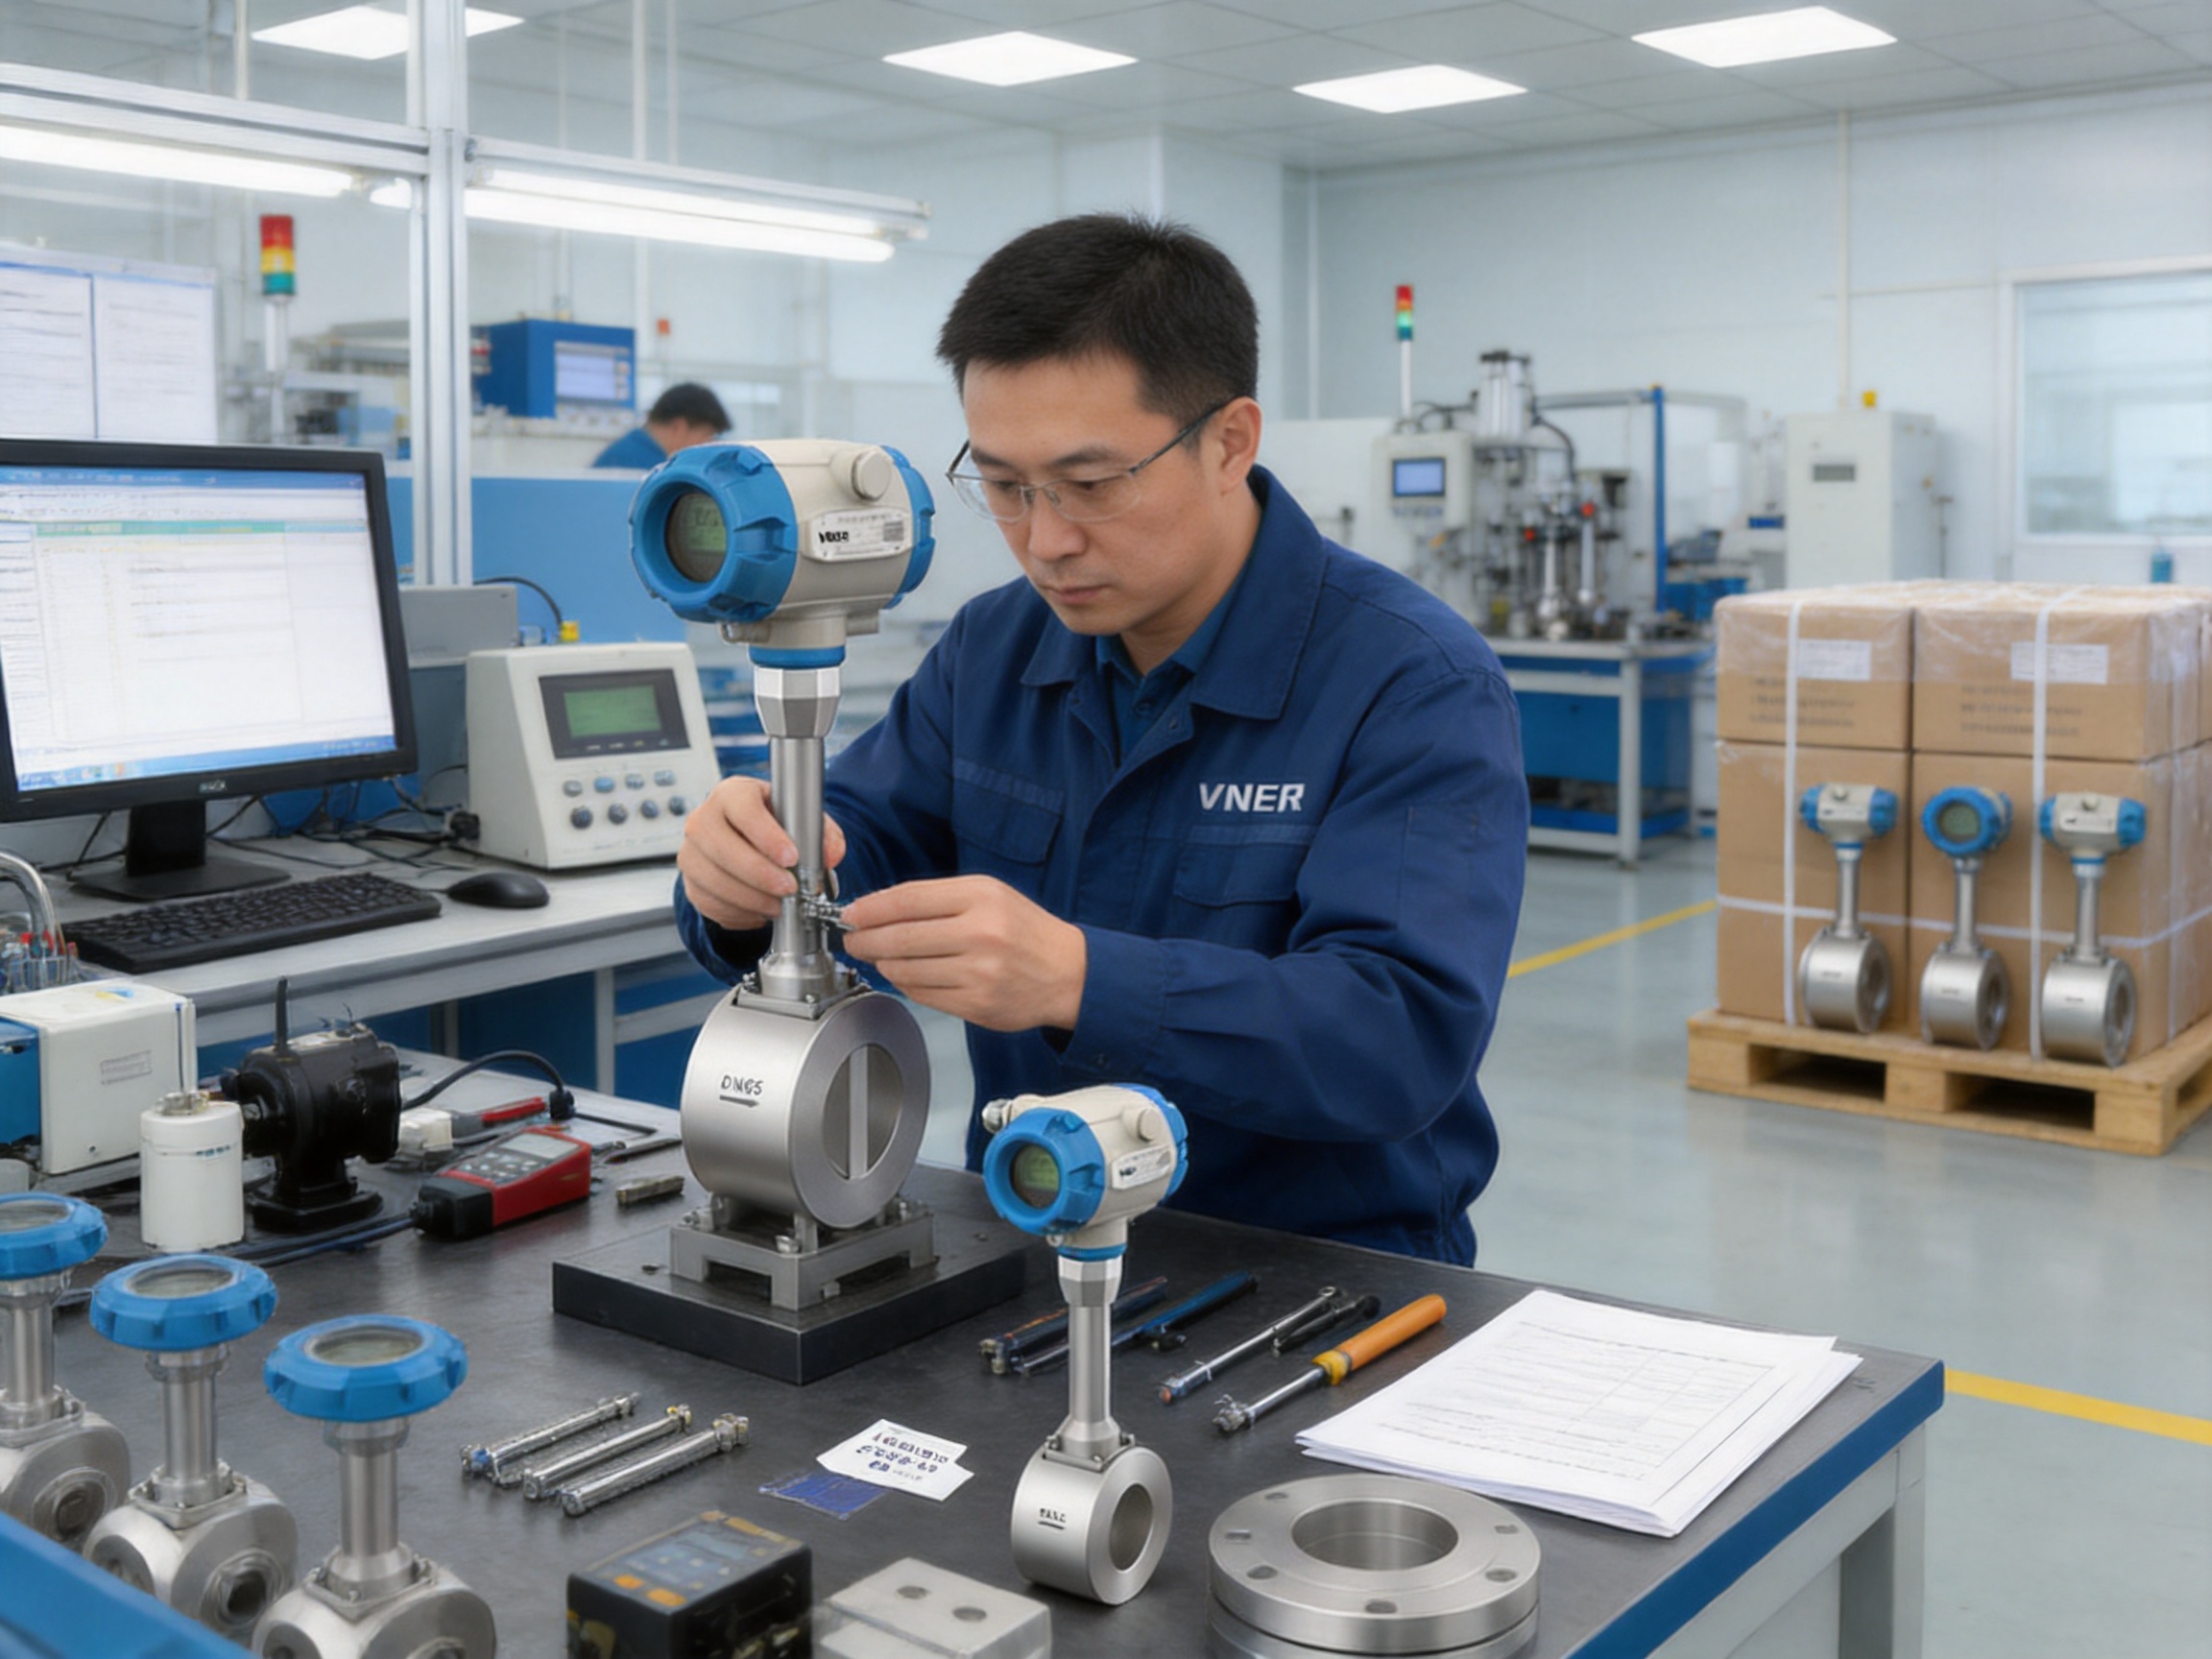
The performance of an industrial flowmeter depends not only on its operating principle but also on how consistently it is manufactured. The MA80T is produced by Jiangsu VNER Electronic Technology Co., Ltd., an industrial flowmeter manufacturer based in Yangzhou, China. Since 2011, the company has developed and supplied electromagnetic, Coriolis, vortex, swirl, turbine, thermal mass, ultrasonic, and metal-tube rotameter solutions.
This broad product experience is valuable because different measurement technologies share many engineering requirements. Sensor design, signal processing, material selection, calibration, enclosure construction, documentation, and application sizing all benefit from knowledge across multiple flowmeter platforms.
The company operates across three plants with approximately 23,000 square meters of facilities and a technical team of more than 150 people. Its experience includes more than 2,000 engineering projects in over 30 countries. These figures indicate a manufacturing and project-support structure capable of serving standard products as well as customized industrial requirements.
Engineering-Driven Product Development
Industrial flowmeters must be designed around real process conditions rather than laboratory conditions alone. Product development therefore requires consideration of pressure, temperature, density, viscosity, vibration, corrosion, electrical interference, installation geometry, and communication requirements.
The MA80T reflects this engineering approach through its application to steam, gases, and liquids; its high-temperature and high-pressure configurations; its flange and wafer options; and its compatibility with horizontal or vertical installation arrangements. The objective is to provide a practical instrument that can be integrated into different plant systems without unnecessary complexity.
Engineering teams can support users by reviewing process data, selecting a suitable meter size, checking velocity, evaluating pressure loss, confirming material compatibility, and determining whether compensation is needed. Such engineering review is particularly important for steam and gas because density varies with pressure and temperature.
In-House Calibration
Calibration is one of the most important stages in flowmeter production. It verifies the relationship between the actual reference flow and the output of the instrument. A controlled calibration process helps detect sensor problems, dimensional deviations, signal-processing errors, and assembly issues before shipment.
In-house calibration can also improve traceability and manufacturing feedback. If a product family shows a systematic deviation, engineering and production teams can investigate the cause and improve the process. Calibration records provide useful documentation for customers, quality departments, and project acceptance procedures.
For users, calibration should be considered part of the complete measurement system rather than an isolated factory activity. Installation conditions, process properties, upstream disturbances, and compensation parameters also influence field performance. Nevertheless, a controlled factory calibration provides an essential baseline for reliable operation.
Automated and Controlled Manufacturing
Increasing automation can improve consistency in assembly, inspection, testing, and data recording. Automated or semi-automated production processes help reduce variation caused by manual operations, particularly where repeated positioning, fastening, soldering, sealing, or electronic testing is involved.
Automation is most effective when combined with process controls, trained personnel, inspection standards, and documented work instructions. Industrial instrument manufacturing requires both precision equipment and experienced engineers who understand how physical construction affects measurement performance.
The company’s focus on increasingly automated manufacturing supports repeatable production and product consistency. This is particularly important for projects that require multiple flowmeters with matching specifications, consistent documentation, and interchangeable maintenance practices.
Quality Systems and Traceability
Traceability allows a manufacturer and user to identify the materials, components, calibration results, inspection steps, and configuration data associated with a particular instrument. This information is important in regulated industries, large EPC projects, and plants where maintenance records must be maintained for many years.
Certified quality processes can support control of incoming materials, component inspection, assembly verification, pressure testing, electrical testing, calibration, final inspection, packaging, and shipment documentation. A strong quality system also provides a structured method for handling nonconformities and customer feedback.
For the MA80T, traceability is especially valuable when meters are installed in high-temperature steam lines, hazardous industrial areas, or critical utility systems. It can help users confirm the original configuration and make informed decisions when replacing electronics, ordering spare parts, or planning recalibration.
Customization and OEM Support
Industrial users often require more than a standard catalog instrument. Projects may specify particular flange standards, pressure classes, electrical connections, display orientations, output protocols, materials, temperature ratings, or installation arrangements. OEM customers may require private labeling, special documentation, or integration with a larger control package.
Jiangsu VNER Electronic Technology Co., Ltd. supports EPC contractors, end users, and OEM partners. This project-oriented capability can be important when a flowmeter must fit a complete process package rather than operate as an independent instrument.
Customization should always preserve the technical limits of the measurement principle. A special connection or enclosure does not automatically make the meter suitable for every process. The best results are obtained when customization begins with a complete process data sheet and a clear definition of performance, environmental, and documentation requirements.
Signal Integration and Operational Data
A modern industrial flowmeter should provide more than a local indication. Flow data may be used by distributed control systems, programmable logic controllers, energy-management platforms, supervisory systems, or plant historians. The MA80T transmitter can be specified for integration with the customer’s control architecture according to the available output and communication requirements.
Real-time flow data supports trend analysis, alarm management, production reporting, utility allocation, and preventive maintenance. Operators can compare flow with pressure, temperature, valve position, pump status, production output, or energy consumption. These comparisons often reveal problems that cannot be identified from a single instantaneous reading.
For example, an increasing steam flow with unchanged production may indicate heat loss or equipment degradation. A falling chilled-water flow may suggest a blocked strainer or pump problem. A gas-flow increase during non-production hours may indicate leakage. The flowmeter becomes more valuable when its data is incorporated into a broader operational strategy.
Maintenance and Lifecycle Management
The MA80T’s no-moving-parts design can reduce routine mechanical maintenance, but periodic inspection remains advisable. Users should check the condition of electrical connections, grounding, cable glands, transmitter housing, display visibility, process flanges, gaskets, and pipe supports.
In dirty services, deposits may form around the shedder bar or inside the flow body. Such deposits can alter the flow geometry and affect measurement. The cleaning method should be compatible with the body material, sensor construction, and process requirements. Any inspection or cleaning procedure must follow plant safety rules and confirm that the line has been isolated, depressurized, drained, and cooled as required.
Calibration intervals depend on application criticality, process conditions, regulatory requirements, historical stability, and the company’s quality program. Critical steam, custody-related, pharmaceutical, or energy-allocation applications may require more frequent verification than general utility monitoring.
Maintaining accurate configuration records is equally important. Changes to process pressure, temperature, gas composition, line size, control strategy, or compensation settings can affect the suitability of the original meter selection. A lifecycle approach should include commissioning records, calibration certificates, maintenance history, process changes, and replacement planning.
Recommended Selection Checklist
Before ordering an MA80T Series Vortex Flowmeter, the user should collect complete process information. The minimum data normally includes the measured medium, normal flow, minimum flow, maximum flow, operating pressure, design pressure, operating temperature, design temperature, line size, line material, connection standard, fluid density, viscosity where applicable, and required output signals.
For gases, the gas composition, molecular weight, compressibility, reference conditions, and expected pressure variation should be specified. For steam, the state of the steam, pressure range, temperature range, dryness or superheat condition, and need for mass or energy compensation should be confirmed.
For liquids, users should provide density, viscosity, conductivity if relevant, solids content, gas entrainment risk, corrosion characteristics, and minimum back pressure. The presence of abrasive particles or high viscosity may indicate that another flowmeter technology is more appropriate.
Installation information should include the upstream and downstream pipe arrangement, nearby elbows or valves, available straight-run length, pipe orientation, ambient temperature, vibration sources, hazardous-area requirements, and accessibility for maintenance.
The project specification should also identify display requirements, alarm functions, output type, communication protocol, enclosure protection, cable entry, calibration documentation, material certificates, inspection plans, and spare-parts expectations. Providing this information early reduces the risk of rework and improves the accuracy of the final configuration.
Frequently Asked Questions
What media can the MA80T Series measure?
The MA80T Series is designed for steam, gases, and liquids. Common applications include saturated steam, superheated steam, natural gas, fuel gas, compressed air, nitrogen, carbon dioxide, hot water, chilled water, condensate, and selected process liquids. The actual suitability depends on flow range, pressure, temperature, cleanliness, viscosity, density, and material compatibility.
Does the meter contain a rotating turbine?
No. The MA80T uses a fixed bluff body to generate alternating vortices and a piezoelectric sensor to detect the vortex frequency. The absence of a rotating measuring element reduces mechanical wear and can simplify maintenance compared with technologies that depend on bearings or rotors.
Can the MA80T measure steam at high temperature?
Applicable configurations are specified for temperatures up to 350°C. The exact allowable temperature depends on the selected model, sensor, connection, electronics, pressure rating, and installation arrangement. The final configuration should be confirmed against the process design conditions before purchase.
What is the maximum pressure capability?
Applicable MA80T configurations are specified for pressures up to 4.0 MPa. The allowable pressure must be checked together with flange rating, body material, temperature, gasket, and connection standard. The highest pressure and temperature should not be evaluated independently.
Can it be installed in a vertical pipe?
Yes, the series supports horizontal and vertical installation when the direction of flow and process conditions are suitable. Liquid lines should remain full, while steam and gas lines should be designed to prevent condensation pockets and unstable flow conditions.
Is pressure and temperature compensation necessary?
Compensation may be necessary when pressure or temperature changes significantly, especially for gases and steam. The requirement depends on whether the user needs actual volumetric flow, standardized volume, mass flow, or thermal-energy information. Application engineers should review the required calculation basis before selecting the transmitter configuration.
How does the MA80T compare with an electromagnetic flowmeter?
An electromagnetic flowmeter is primarily intended for conductive liquids and is often preferred for water, wastewater, and slurry applications. The MA80T can measure steam and gases as well as selected liquids, making it more versatile for facilities that need one technology across multiple utility services. For highly conductive liquids with solids, an electromagnetic meter may still be the better choice.
How does the MA80T compare with a Coriolis meter?
A Coriolis meter directly measures mass flow and may also provide density and temperature. It is valuable for high-accuracy batching and process-material measurement. The MA80T is generally a more practical option for large utility lines, steam networks, compressed air, and general gas monitoring where direct Coriolis mass measurement is not required.
What causes unstable vortex readings?
Possible causes include flow below the minimum measurement range, excessive vibration, poor straight-run conditions, upstream swirl, two-phase flow, gas entrainment in liquids, condensation in steam lines, pulsating flow, incorrect grounding, and improper transmitter configuration. Reviewing the installation and process conditions is usually the first troubleshooting step.
What manufacturing support is available?
The manufacturer provides engineering-driven sizing and selection, in-house calibration, certified quality processes, project support, customization, and OEM cooperation. The company serves EPC contractors, end users, and industrial partners across oil and gas, petrochemical, power, water and wastewater, chemical, pharmaceutical, and other process industries.
How often should the flowmeter be recalibrated?
The interval depends on the application, regulatory requirements, criticality, process conditions, historical performance, and customer quality procedures. General utility applications may use a risk-based interval, while pharmaceutical, energy-allocation, or critical process applications may require more frequent verification.
Conclusion
The MA80T Series Vortex Flowmeter provides a robust and flexible solution for industrial measurement of steam, gases, and liquids. Its Kármán vortex operating principle, piezoelectric detection, fixed internal structure, and lack of rotating measuring components support stable performance and reduced mechanical maintenance. High-temperature and high-pressure capability, low pressure drop, and flange or wafer installation options further expand its usefulness across industrial facilities.
Compared with turbine, electromagnetic, Coriolis, differential-pressure, and ultrasonic technologies, the MA80T offers a distinctive balance of medium flexibility, construction simplicity, and suitability for utility measurement. It is particularly attractive for steam networks, fuel-gas systems, compressed-air distribution, hot-water and chilled-water loops, process utilities, and energy-management projects.
The value of the instrument also depends on the manufacturing and engineering system behind it. Jiangsu VNER Electronic Technology Co., Ltd. combines multi-technology flowmeter experience with in-house calibration, quality control, traceability, project engineering, modern production facilities, and support for EPC and OEM requirements. These capabilities help convert a standard flowmeter principle into a dependable industrial product that can be specified, manufactured, calibrated, installed, and maintained with greater consistency.
For the best result, users should treat flowmeter selection as an engineering task. Accurate process data, correct sizing, suitable installation, compensation where required, effective commissioning, and lifecycle verification are all necessary. When these elements are addressed together, the MA80T can provide dependable real-time flow information for process control, energy optimization, production management, and long-term plant improvement.
References
1. International Organization for Standardization. Measurement of Fluid Flow in Closed Conduits: General Principles and Flowmeter Selection.
2. International Organization for Standardization. Measurement of Fluid Flow by Means of Pressure Differential Devices.
3. International Organization for Standardization. Measurement of Fluid Flow in Closed Conduits: Vocabulary and Symbols.
4. American Society of Mechanical Engineers. Flow Measurement Engineering Practices for Industrial Process Systems.
5. International Electrotechnical Commission. Industrial-Process Measurement and Control Equipment: Environmental and Electrical Requirements.
6. Industrial Instrumentation Engineering. Principles of Vortex Shedding Flow Measurement and Strouhal Number Applications.
7. Steam System Engineering. Steam Distribution, Condensate Management, Energy Accounting, and Flow Measurement.
8. Process Measurement and Control Handbook. Comparative Selection of Vortex, Turbine, Electromagnetic, Coriolis, Differential-Pressure, and Ultrasonic Flowmeters.
Product: MA80T Series Vortex Flowmeter-副本
Products
Contact Information
-

+86 18652789521
+86-0514-83633600 / 83633900 -

+86-0514-83633600 / 83633900
-

s@vner.com.cn
katherine@vner.com.cn -

No. 11 Xingye Road, Chenji Town Industrial Park, Yizheng, Yangzhou, China
