 0
 EN
 English
 عربى
 Español
 русский
If you need any help, please feel free to contact us
Home / Author / Ding Yuchun — Overseas After-Sales Support Engineer / MA80T Series Vortex Flowmeter: Reliable Measurement for Steam, Gas, and Clean Liquids
MA80T Series Vortex Flowmeter: Reliable Measurement for Steam, Gas, and Clean Liquids
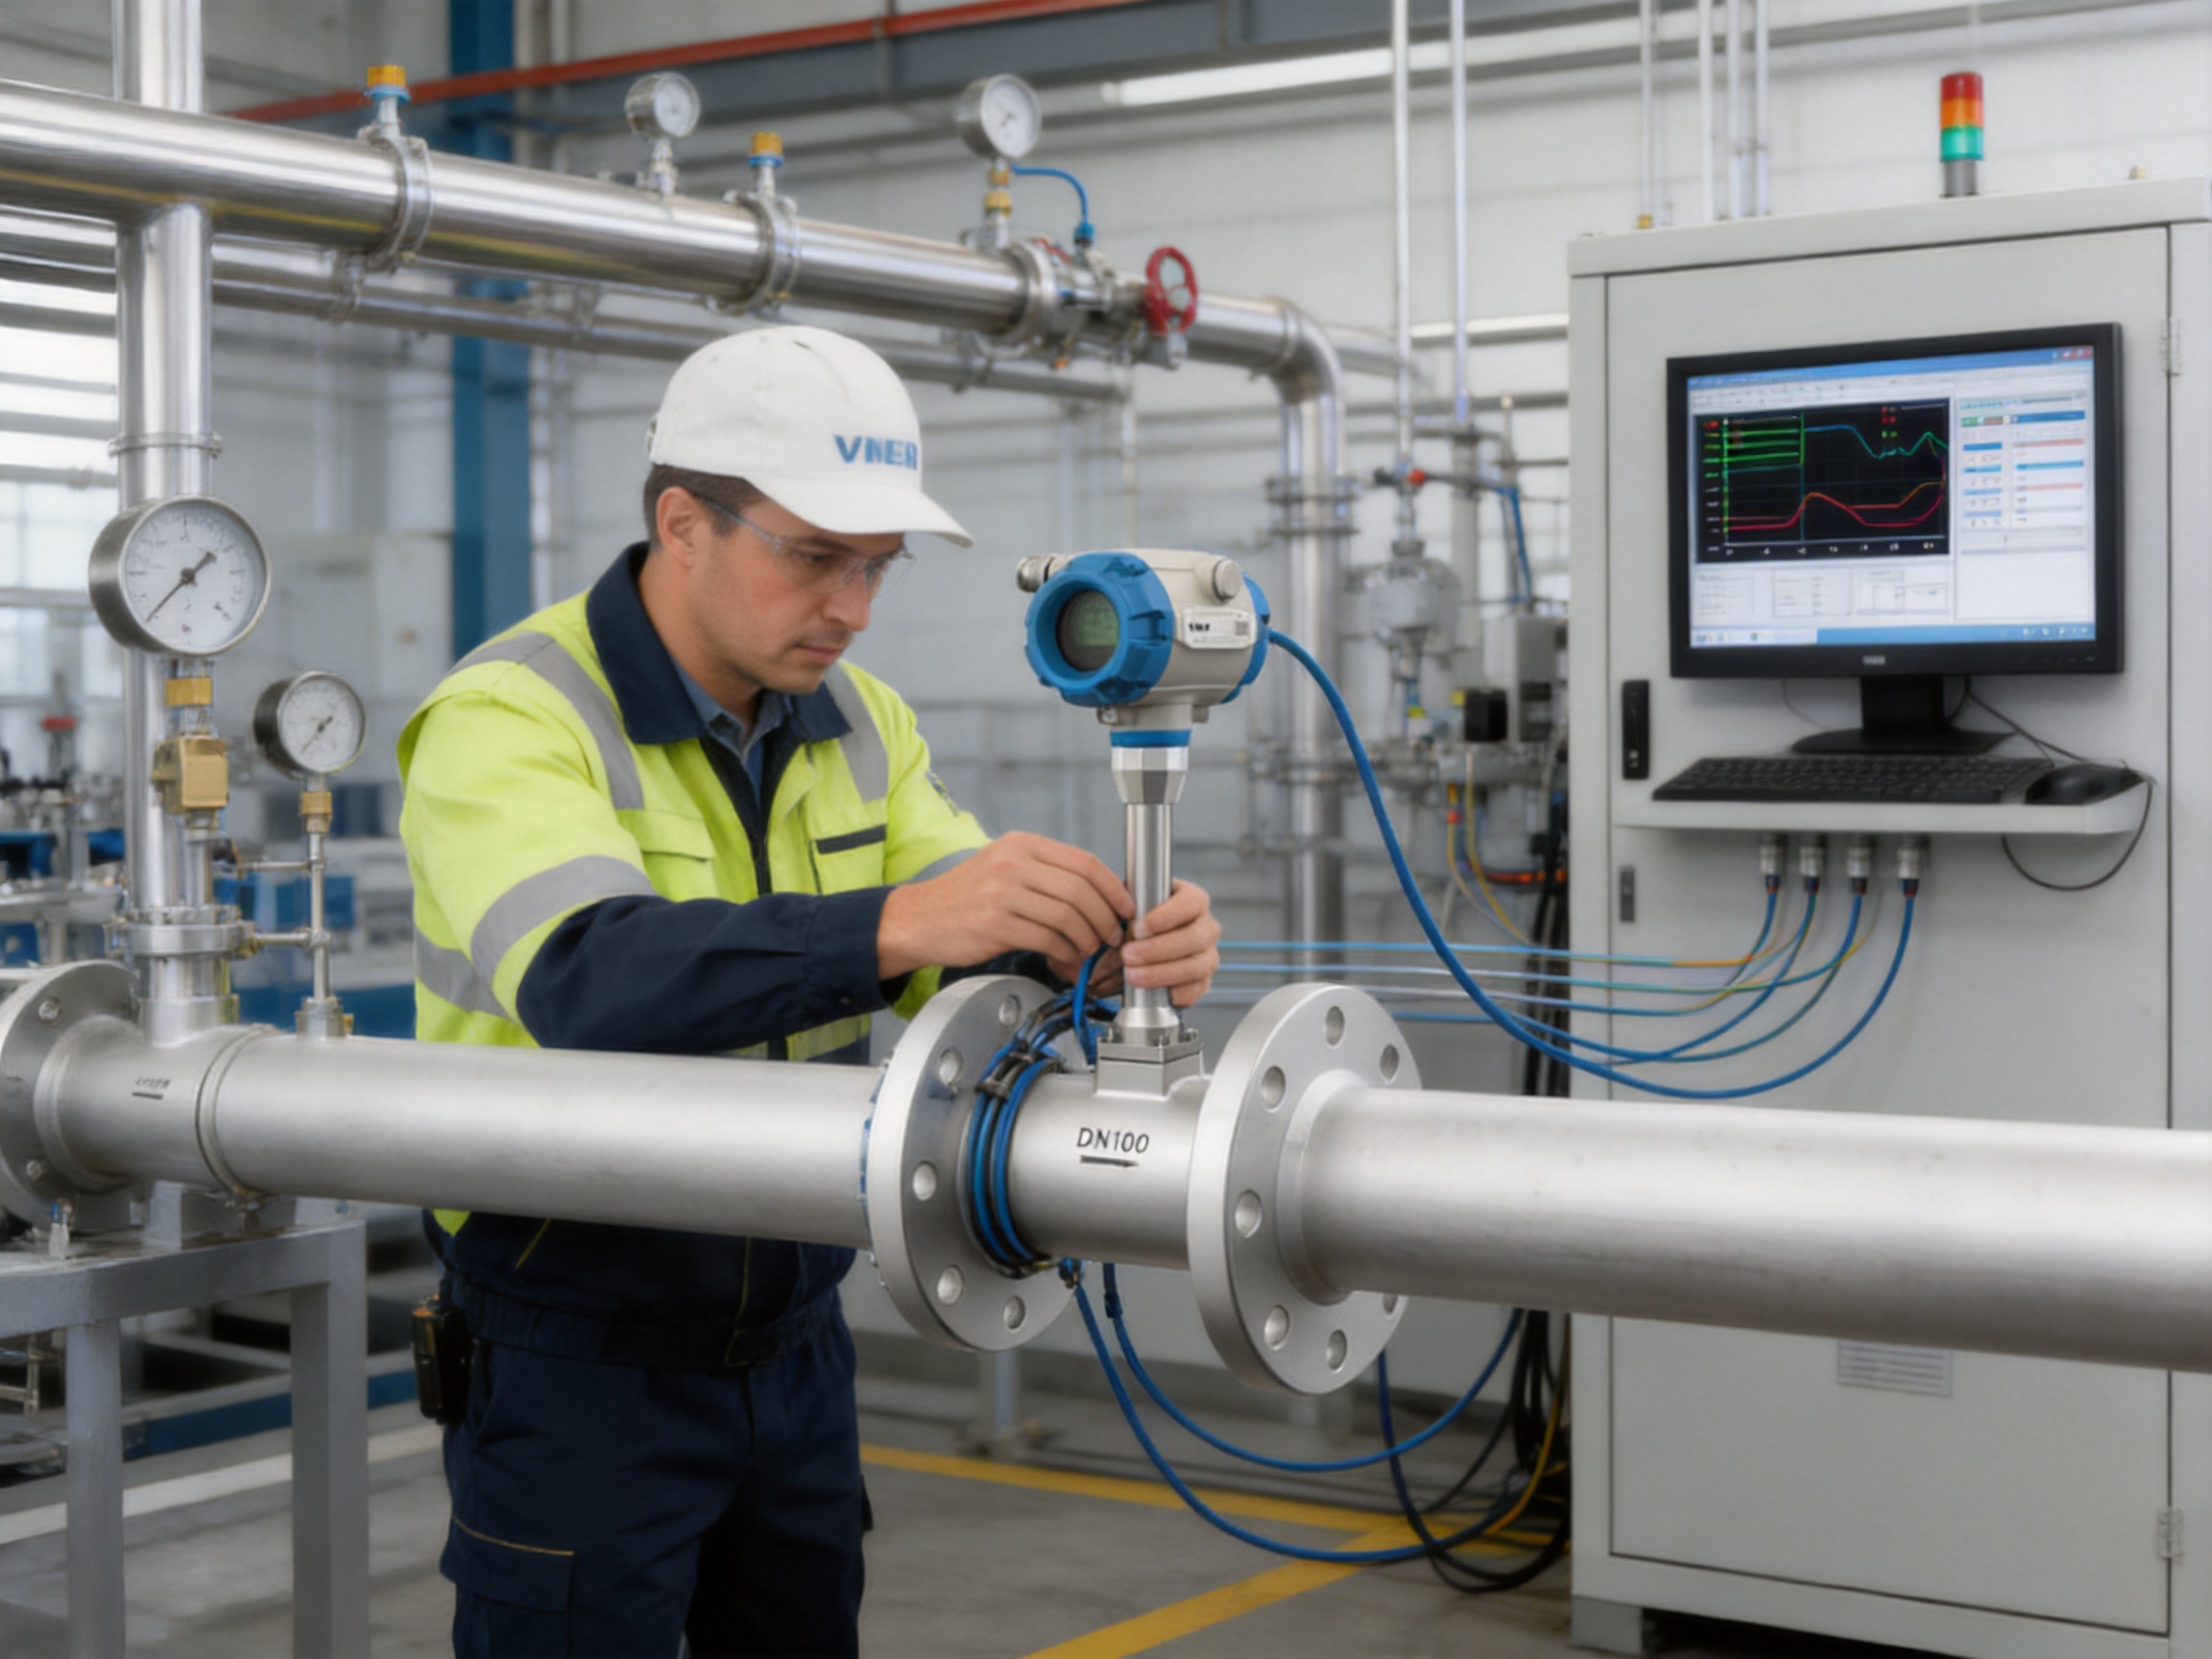
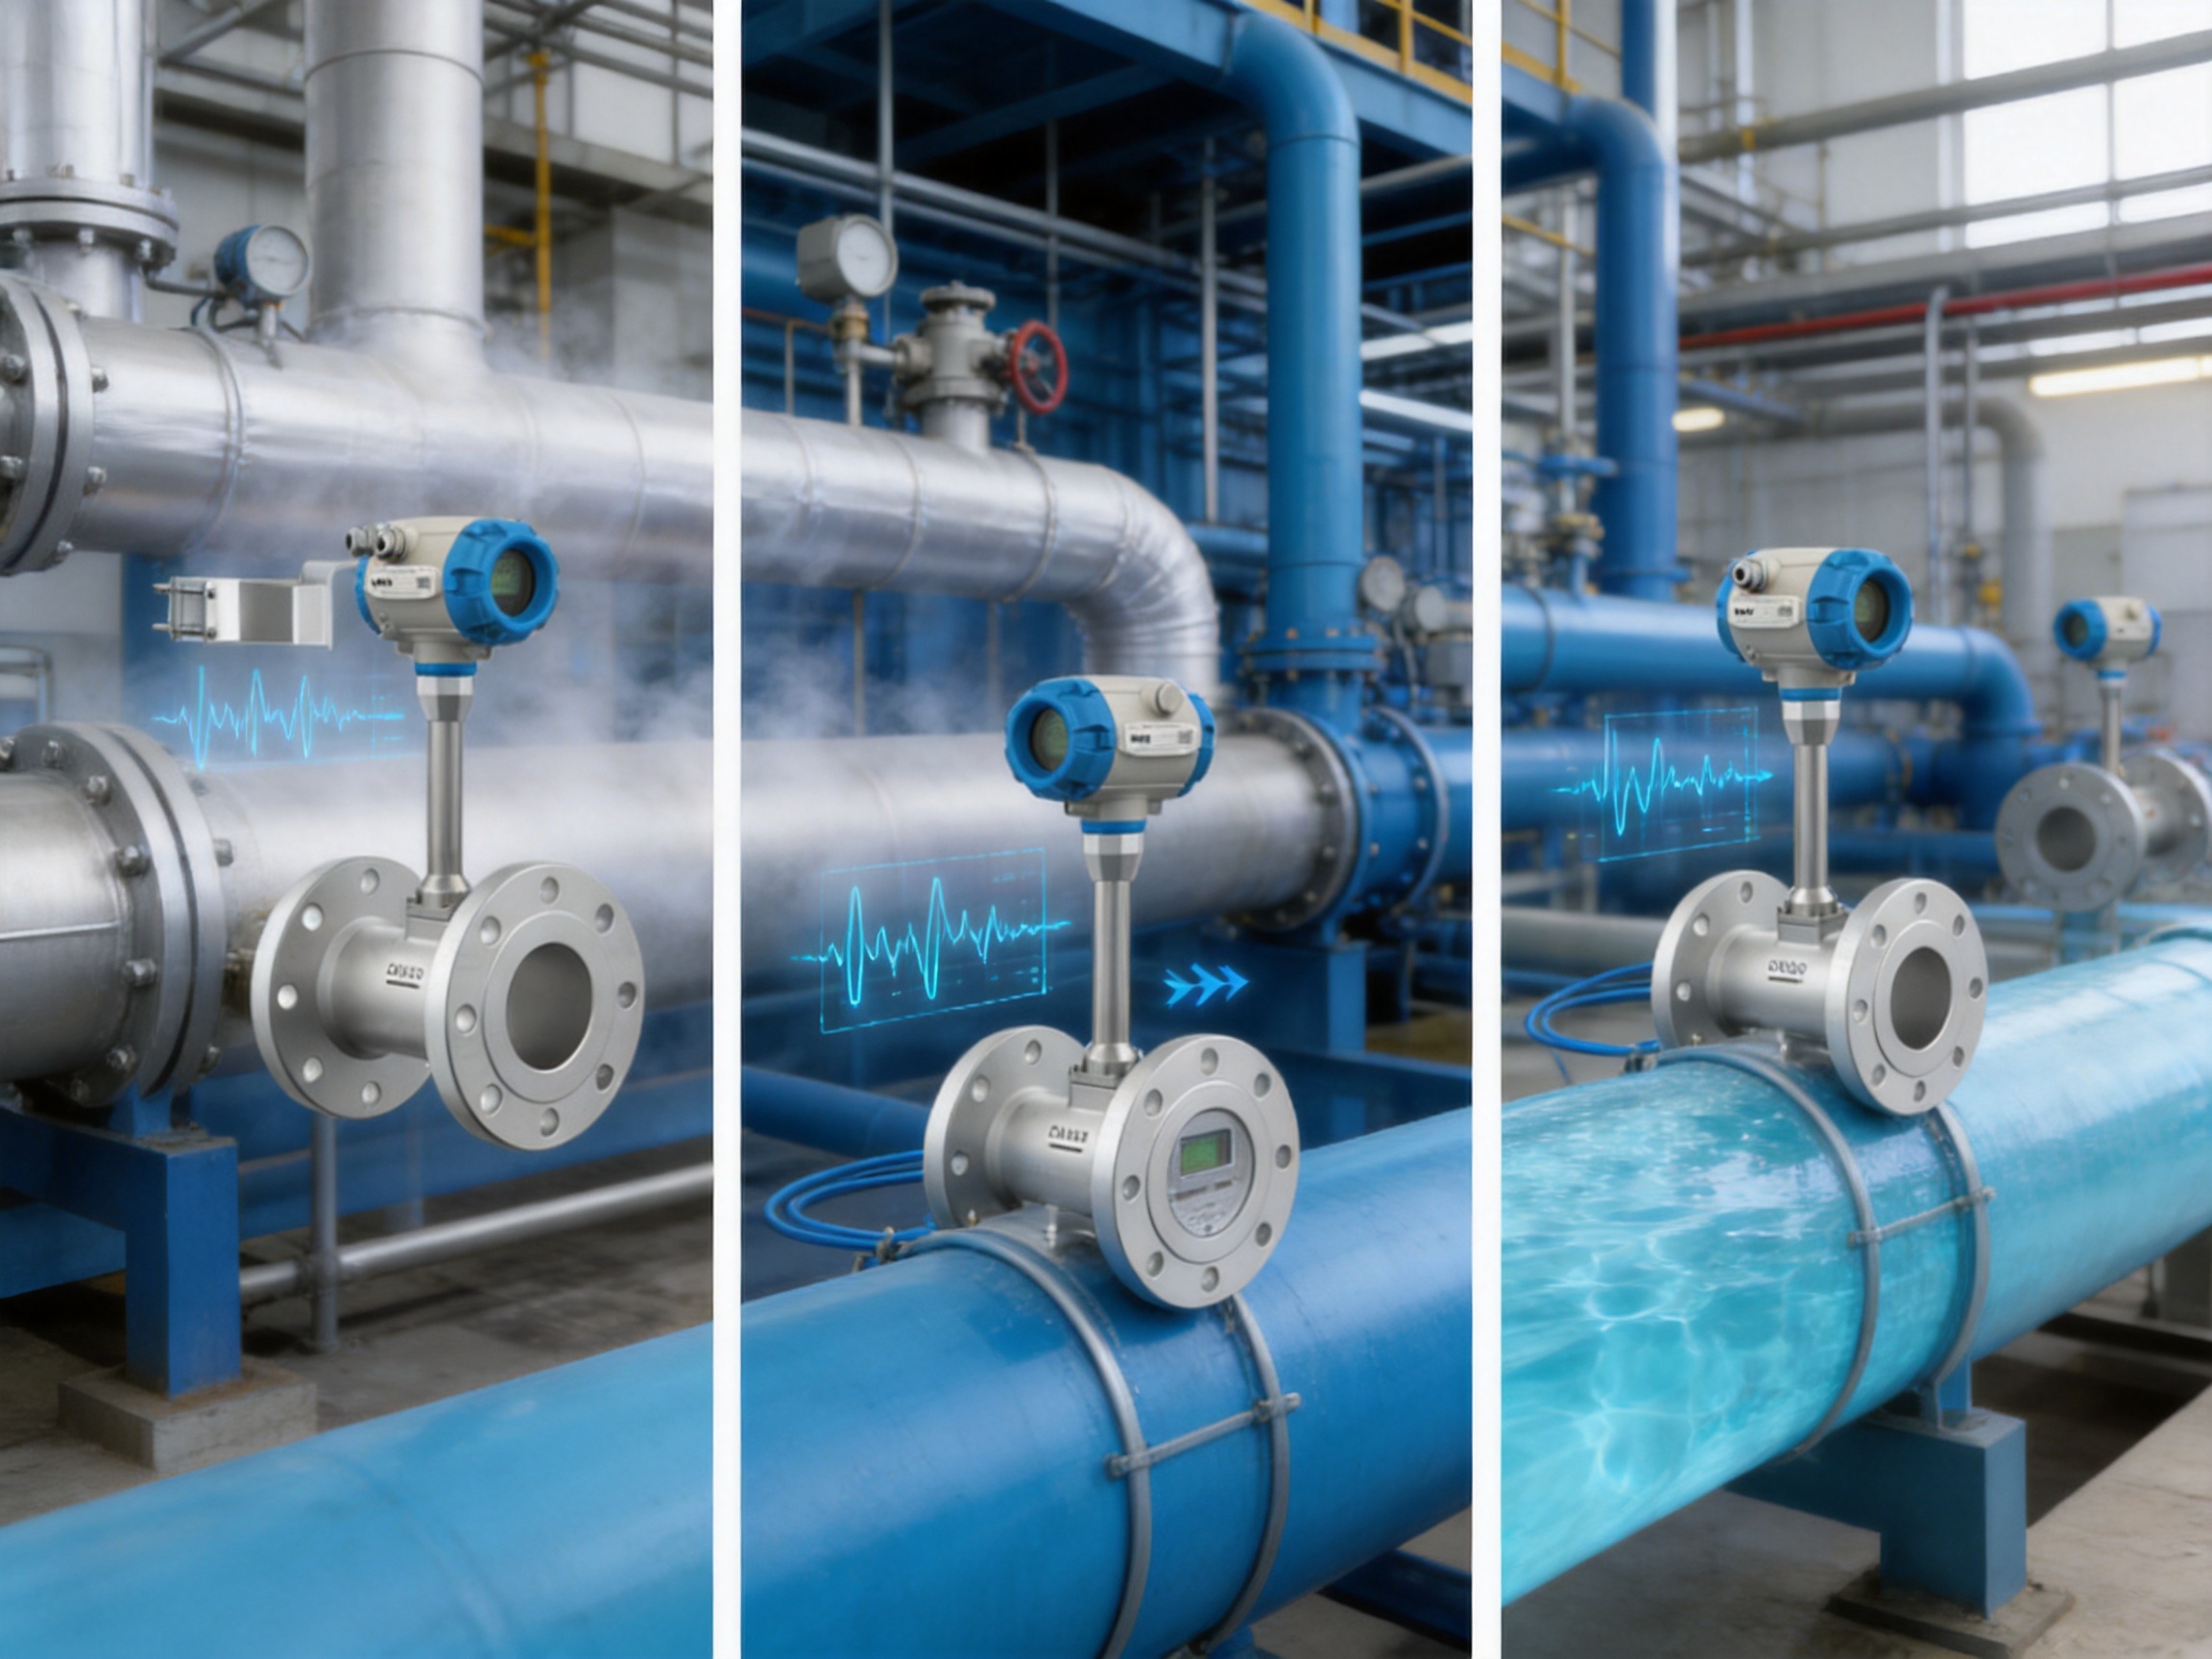
Industrial plants depend on accurate and stable flow measurement to control production, manage energy consumption, protect equipment, and verify process performance. Steam distribution, compressed-air networks, natural-gas supply, utility water systems, and clean process-liquid lines all require instruments that can operate continuously under changing pressure, temperature, and flow conditions. The MA80T Series Vortex Flowmeter is designed for these duties, combining the established Kármán vortex measurement principle with a robust flow body, piezoelectric sensing, flexible process connections, and industrial communication options.
The MA80T is suitable for measuring saturated steam, superheated steam, gases, and clean or low-viscosity single-phase liquids. Its design contains no moving parts, reducing mechanical wear and routine maintenance compared with many traditional mechanical flowmeters. At the same time, the meter provides practical accuracy, broad application coverage, and real-time output for integration with distributed control systems, programmable logic controllers, energy-management platforms, and plant-monitoring software.
Manufactured by Jiangsu Vner Electronic Technology Co., Ltd., the MA80T is supported by engineering-based product selection, in-house calibration, quality control, and application experience across multiple industrial sectors. The manufacturer’s broader portfolio includes electromagnetic, Coriolis, vortex, swirl, turbine, thermal mass, ultrasonic, and metal-tube rotameter technologies. This range enables the company to recommend the most appropriate measuring principle for a particular medium rather than treating every application as a one-product solution.
What Is a Vortex Flowmeter?
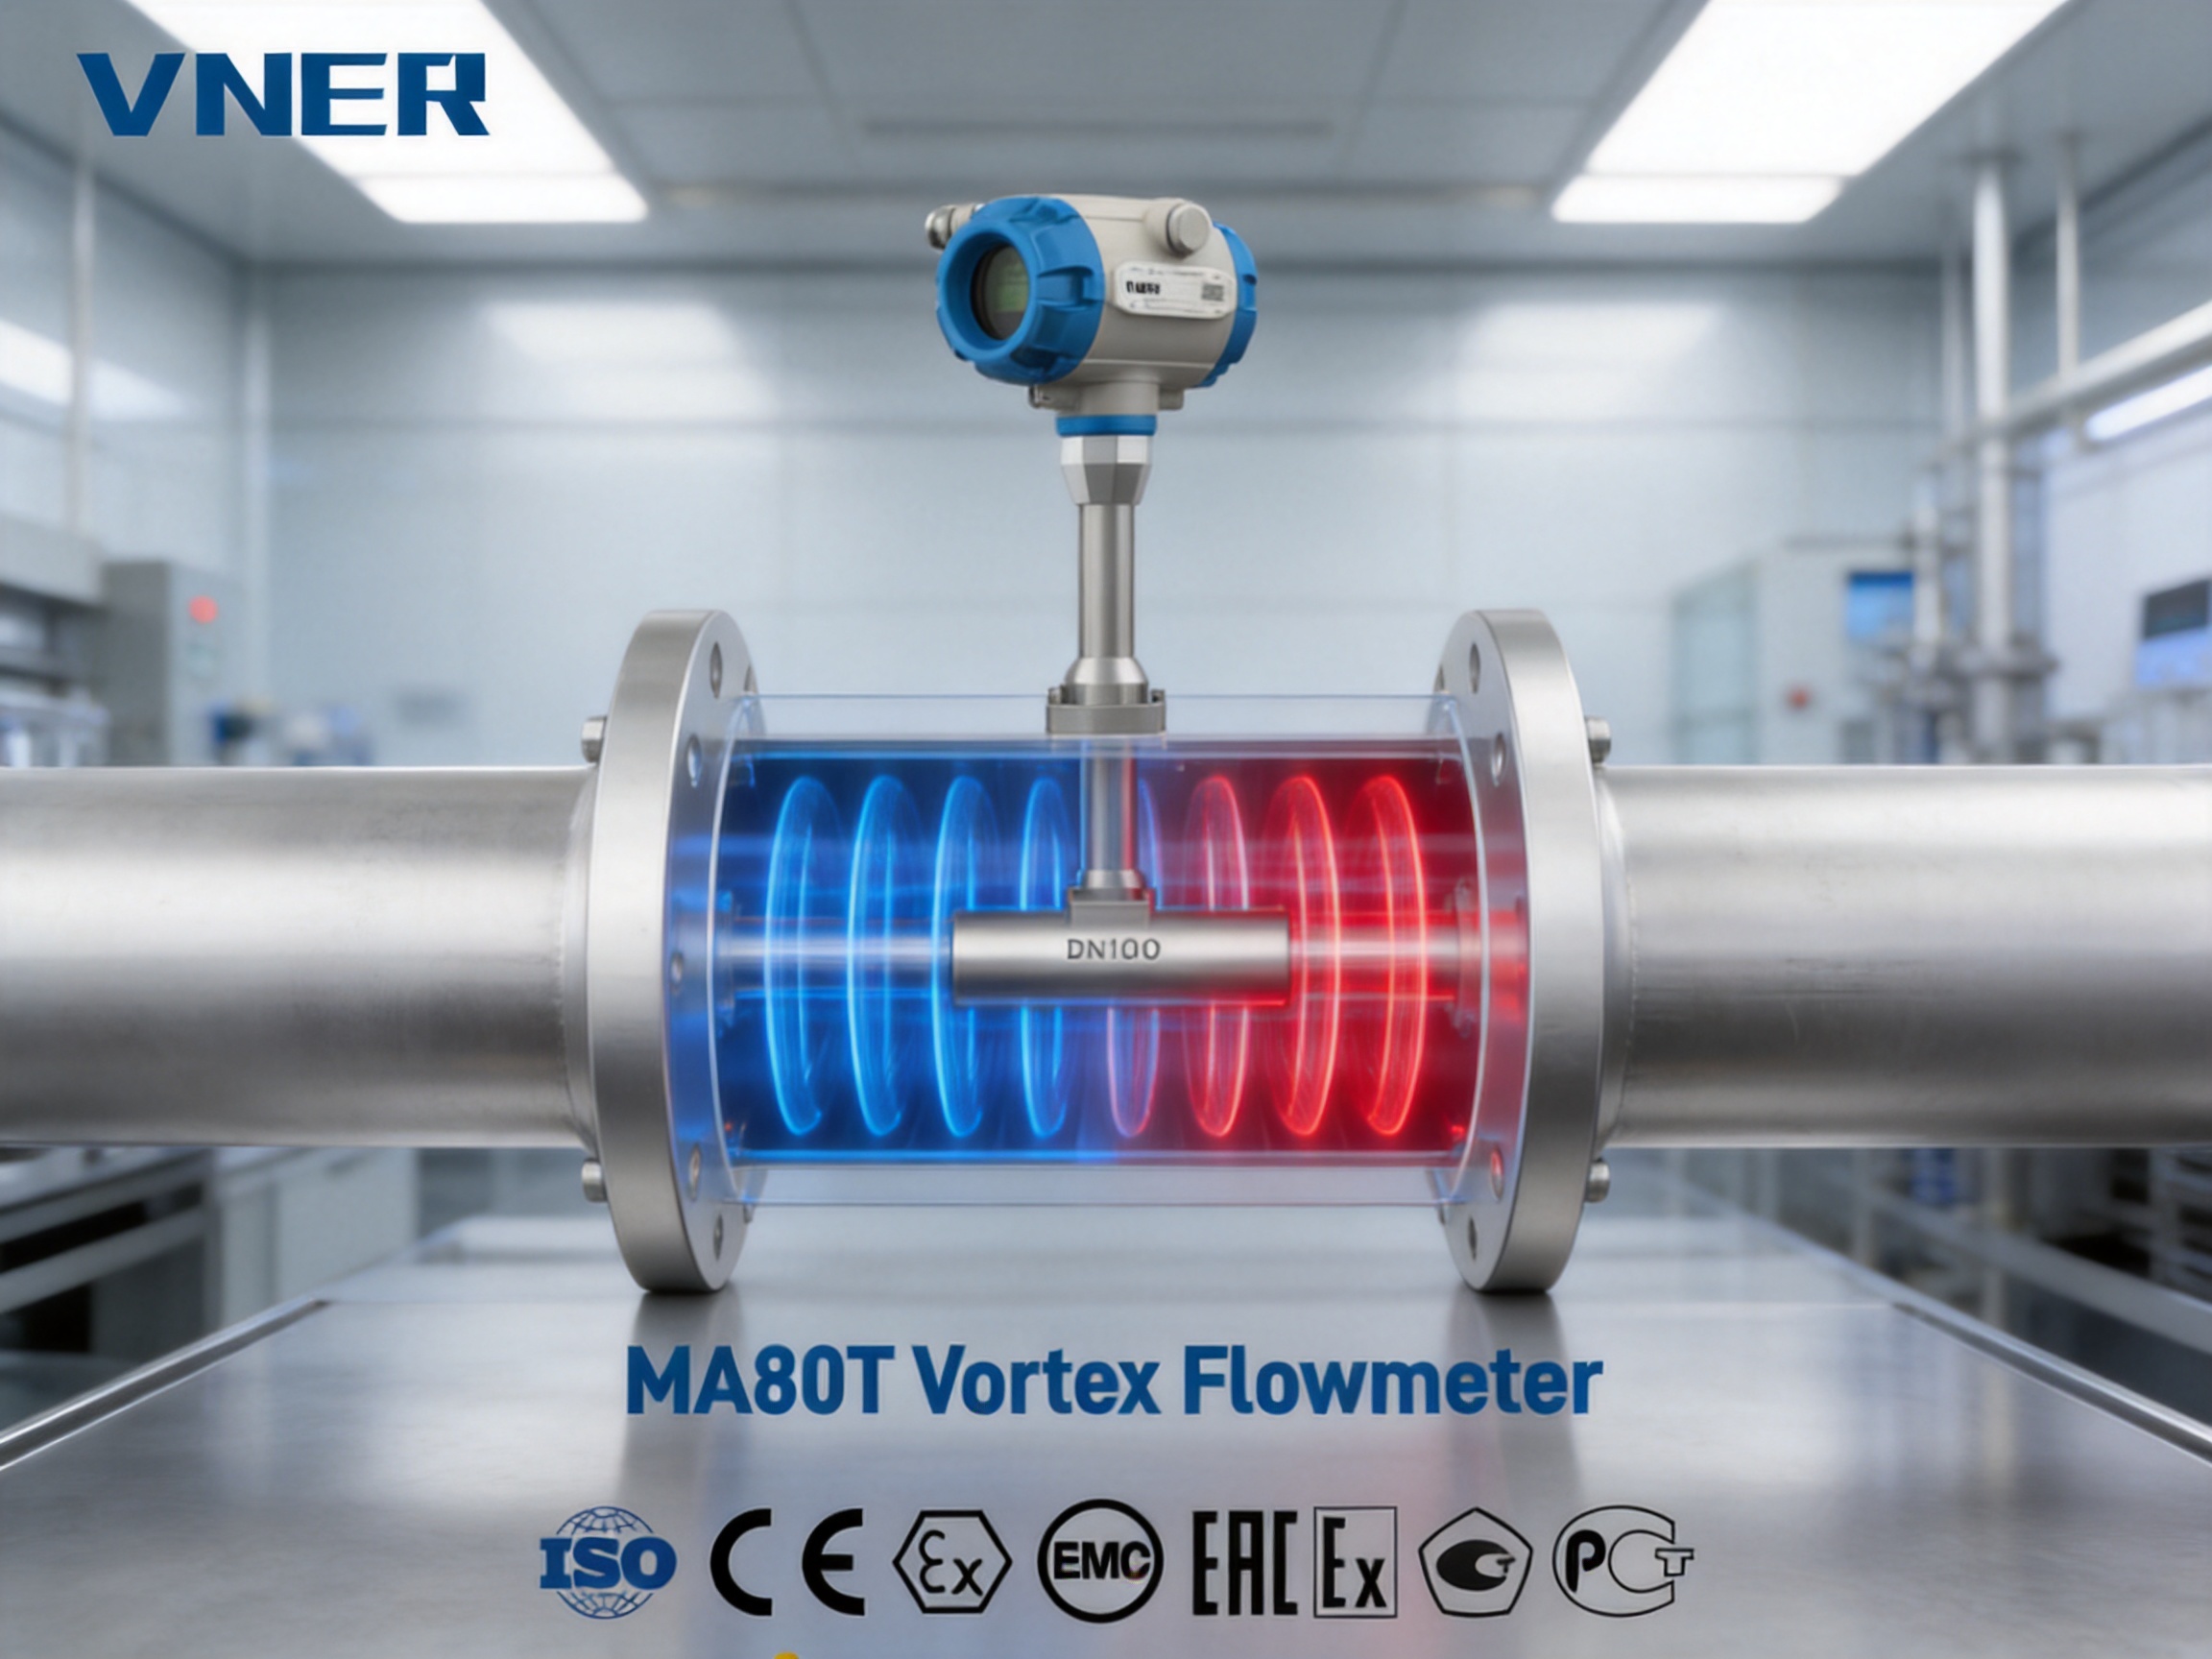
A vortex flowmeter measures flow by detecting the alternating vortices generated when a fluid passes a fixed obstruction known as a bluff body or shedder bar. This phenomenon is called a Kármán vortex street. As the fluid moves downstream, vortices are released alternately from opposite sides of the bluff body. Within the suitable operating range, the frequency of vortex shedding is proportional to the average velocity of the fluid.
The MA80T uses a piezoelectric sensor to detect the pressure fluctuations or mechanical effects associated with vortex formation. Its electronics process the detected signal and convert the vortex frequency into a flow-rate value. Depending on the configuration, the instrument can provide a current output, pulse output, local indication, and optional digital communication.
The relationship between vortex frequency and flow velocity is commonly expressed through the Strouhal relationship. In simplified form, the vortex frequency depends on the Strouhal number, the flow velocity, and the characteristic dimension of the bluff body. The meter’s electronics and calibration data use this relationship to calculate flow. Because the shedder bar is fixed and the sensing element has no rotating shaft, impeller, or gear train, the measurement principle is mechanically simple and well suited to continuous industrial service.
Vortex meters are particularly useful where the same instrument may be required to measure steam, compressed air, nitrogen, fuel gas, natural gas, or clean water. They are also commonly selected for utility metering, boiler systems, process heating, and energy-management applications. Correct sizing, adequate straight-run piping, suitable fluid conditions, and proper installation remain essential for achieving the best performance.
Operating Principle of the MA80T
When the process medium enters the MA80T body, it flows around the internal bluff body. At sufficiently high Reynolds numbers, the flow separates from the sides of the shedder bar and generates a regular alternating vortex pattern. Each vortex produces a small but measurable pressure disturbance. The piezoelectric sensor detects these disturbances and sends a signal to the signal-processing electronics.
The electronics distinguish the vortex signal from background vibration and process noise. The resulting frequency is converted into volumetric flow. If pressure and temperature compensation are included in the selected system, the measured value may also be used for compensated gas or steam calculations. The available output formats allow the value to be transmitted to a control room, recorded by an energy-management system, or used directly for alarm and control functions.
The measurement principle is suitable for single-phase media with appropriate flow conditions. Saturated steam, superheated steam, clean air, nitrogen, inert gas, fuel gas, natural gas, condensate, utility water, and certain clean low-viscosity liquids are common examples. Applications involving severe multiphase flow, heavy solids, strong pulsation, excessive vibration, or very low Reynolds numbers require careful evaluation before selection.
Unlike a turbine meter, the MA80T does not depend on a rotor turning at a speed proportional to flow. Unlike an electromagnetic flowmeter, it does not require the medium to be electrically conductive. Unlike a Coriolis meter, it does not generally measure mass flow directly through vibrating tubes. Instead, it provides a practical and economical volumetric-flow solution for a broad range of gases, steam, and liquids.
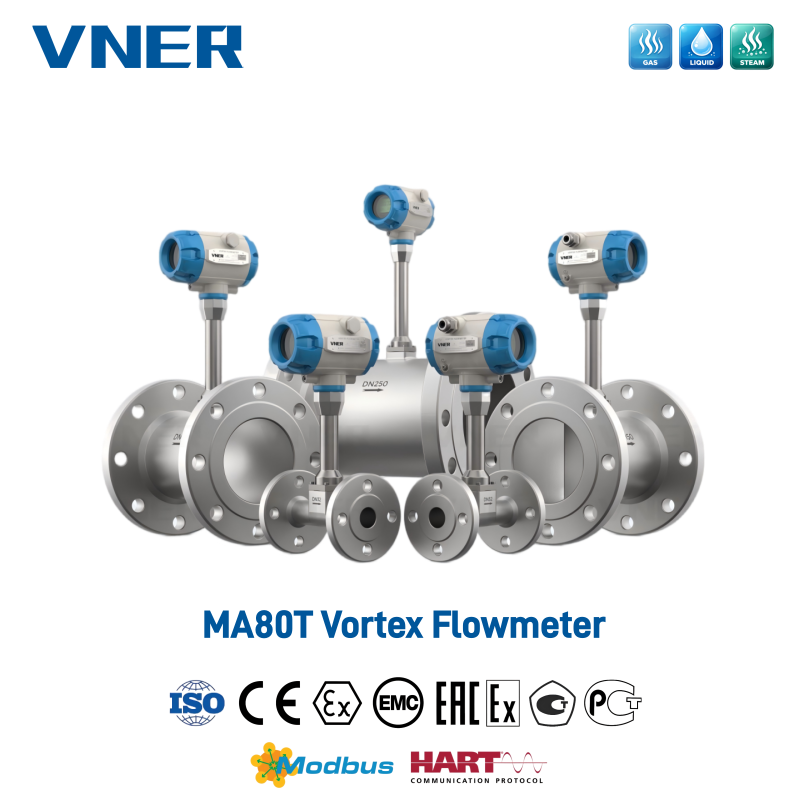
MA80T Series Vortex Flowmeter
Core Technical Characteristics
The MA80T Series is configured for industrial piping systems and can be supplied in flanged or wafer versions. Body and flange materials include SS304 and SS316L, with other materials available according to application requirements. Depending on the model, wetted sensor materials may include SS304, SS316L, Hastelloy C, Hastelloy B, or titanium.
The standard temperature capability is up to approximately 250 °C, while high-temperature versions can reach up to approximately 350 °C. The pressure rating may reach up to 4.0 MPa for suitable models. Exact limits depend on the selected body size, connection configuration, material, electronics, and installation conditions. Application-specific confirmation should always be obtained before ordering.
| Item | MA80T Series Characteristic |
|---|---|
| Measurement principle | Kármán vortex street with piezoelectric detection |
| Measured media | Saturated steam, superheated steam, gases, and clean or low-viscosity liquids |
| Body and flange materials | SS304, SS316L, and optional materials upon request |
| Sensor wetted materials | SS304, SS316L, Hastelloy C, Hastelloy B, or titanium, depending on model |
| Typical liquid accuracy | Up to ±1.0% of rate under calibrated conditions |
| Typical gas and steam accuracy | ±1.0% to ±1.5% of rate under calibrated conditions |
| Typical turndown | Approximately 1:10 to 1:20, depending on medium and installation |
| Temperature capability | Standard versions up to approximately 250 °C; high-temperature versions up to approximately 350 °C |
| Pressure rating | Up to approximately 4.0 MPa for applicable models |
| Process connections | Flanged and wafer configurations |
| Communication options | 4–20 mA, pulse, HART, and Modbus RTU options |
The figures in the table describe typical capabilities rather than a universal specification for every nominal diameter and configuration. Flow range, accuracy, pressure rating, temperature limit, and materials should be confirmed against the final model selection and process data.
Advantages of the MA80T Design
No Moving Parts
A principal advantage of the MA80T is its non-mechanical sensing arrangement. The meter does not use a rotating impeller, bearings, gears, or mechanical transmission parts. This reduces wear caused by continuous operation and helps minimize maintenance requirements. The absence of moving parts is especially valuable in utility systems that operate around the clock and in locations where instrument access is difficult.
Mechanical simplicity also improves long-term repeatability. A turbine meter can be affected by bearing condition, rotor fouling, or changes in friction. A mechanical positive-displacement meter may require inspection of internal moving elements. The MA80T instead relies on the stable geometry of the flow body and the electronic detection of vortex frequency. This makes it well suited to permanent installation in plant utility networks.
Broad Medium Compatibility
The MA80T can be used with steam, gas, and selected liquids. This broad compatibility makes it attractive to plants that need a common measurement platform across different utility systems. A facility may use the meter on boiler steam, compressed air, nitrogen, fuel gas, and clean water, provided each application satisfies the required flow, pressure, temperature, and installation conditions.
Because vortex measurement does not require electrical conductivity, it can measure gases and steam that cannot be handled by electromagnetic meters. It also avoids the rotor-related limitations associated with many turbine meters. For clean, single-phase media, the MA80T offers a useful balance between application flexibility and instrument simplicity.
Industrial Temperature and Pressure Capability
Steam and process-gas applications frequently involve elevated temperature and pressure. The MA80T is available in configurations suitable for standard steam systems and higher-temperature duties. High-temperature versions can be selected for applications approaching 350 °C, while pressure-rated models can support process pressures up to approximately 4.0 MPa.
These capabilities support boiler-room monitoring, steam distribution, process heating, heat recovery, burner fuel measurement, and other demanding applications. The correct instrument configuration is essential. Temperature and pressure limits are influenced by the meter body, flange rating, sensor construction, gasket selection, electronics arrangement, and ambient conditions.
Practical Accuracy and Turndown
Under calibrated conditions, the MA80T can achieve typical liquid accuracy up to ±1.0% of rate. For gases and steam, typical accuracy is approximately ±1.0% to ±1.5% of rate, depending on model and application. A typical turndown range of 1:10 to 1:20 allows one meter to cover a useful operating span without requiring frequent range changes.
Actual performance depends on fluid density, Reynolds number, pipe configuration, vibration, flow profile, sizing, and signal quality. Vortex meters generally require a minimum flow velocity for reliable vortex formation. Selecting a meter that is too large may produce an inadequate signal at low flow, while selecting one that is too small may create unnecessary pressure loss or exceed the allowable velocity at peak flow. Engineering-based sizing is therefore more important than simply matching the line size.
Flexible Industrial Integration
Standard 4–20 mA and pulse outputs allow straightforward integration with PLCs, DCS systems, totalizers, data loggers, and energy-monitoring systems. HART and Modbus RTU options provide additional access to configuration, diagnostic information, measured values, and status data.
Digital communication is valuable during commissioning and maintenance. Technicians can review signal quality, confirm configuration values, identify sensor faults, and support remote troubleshooting without disconnecting the instrument from the process. The available diagnostics include signal-quality monitoring, sensor fault indication, and basic self-check functions.
Comparison with Other Flow Measurement Technologies
Industrial flowmeters are not interchangeable in every application. Each technology has specific strengths. The MA80T’s advantages are most apparent when the medium is a clean gas, steam, or liquid; the process requires a rugged fixed-body instrument; and the plant values low maintenance and flexible installation.
Vortex Flowmeter Versus Turbine Flowmeter
Turbine meters measure flow through rotor speed. They can provide good accuracy for clean liquids and gases, but their performance depends on the condition of the rotor, shaft, and bearings. Contamination, particles, excessive viscosity, or flow disturbances can influence the rotor and increase maintenance requirements.
The MA80T has no rotor or bearings, which can improve durability in continuous utility service. It is also more naturally suited to steam measurement, where a rotating mechanism may be exposed to high temperature and demanding conditions. However, turbine meters may be preferred in certain clean-liquid applications requiring high resolution at lower flow rates. Selection should be based on the actual medium and operating envelope.
Vortex Flowmeter Versus Electromagnetic Flowmeter
Electromagnetic flowmeters are excellent for conductive liquids, slurries, wastewater, and corrosive fluids when the liner and electrode materials are correctly selected. They have no obstruction in the flow tube and can measure many difficult liquid applications. However, they cannot measure nonconductive liquids, most gases, or steam.
The MA80T extends measurement capability to gases and steam without requiring electrical conductivity. It can therefore serve compressed-air, nitrogen, natural-gas, and steam systems where an electromagnetic meter is unsuitable. For conductive liquids containing solids or for very low-velocity liquid duties, an electromagnetic meter may remain the better choice.
Vortex Flowmeter Versus Coriolis Mass Flowmeter
Coriolis meters directly measure mass flow and can also provide density and temperature information. They offer excellent accuracy and are widely used for custody transfer, batching, dosing, and high-value process fluids. Their disadvantages may include higher purchase cost, greater weight, larger installation loads, and increased pressure loss in some sizes.
The MA80T measures volumetric flow and is generally a more economical choice for plant utility systems. For steam, compressed air, fuel gas, and general utility measurement, a vortex meter may provide the required performance without the cost and mechanical mass of a Coriolis meter. Where direct mass measurement, density measurement, or high-precision batching is essential, Coriolis technology may be preferable.
Vortex Flowmeter Versus Thermal Mass Flowmeter
Thermal mass flowmeters are commonly used for gases, especially compressed air, nitrogen, and other clean utility gases. They can measure mass flow without separate pressure and temperature compensation in many configurations. They are often selected for small pipe sizes and low-flow gas monitoring.
The MA80T offers a different solution for gas, steam, and liquid service and can be used in larger industrial piping systems. It is also suitable for steam, while thermal mass meters are generally gas instruments. For gas applications where temperature, pressure, contamination, or installation conditions may affect heat-transfer measurement, vortex technology can offer a robust alternative.
Vortex Flowmeter Versus Ultrasonic Flowmeter
Ultrasonic flowmeters measure the travel-time difference or Doppler effect of sound waves. Clamp-on ultrasonic meters can be installed without cutting the pipe, which is useful for temporary surveys and retrofit projects. Inline ultrasonic meters can offer low pressure loss and broad measurement capability.
The MA80T provides a compact inline solution with a defined flow body and a well-established industrial signal. It is often easier to standardize across steam and gas utility systems. Ultrasonic meters may be more appropriate where nonintrusive installation, very low pressure loss, or large-diameter pipe measurement is the primary objective.
Applications in Steam Systems
Steam is one of the most important applications for vortex flow measurement. Plants need to know how much steam is generated, distributed, consumed, returned, or used in individual process areas. The MA80T can be installed in boiler outlets, main steam headers, branch lines, process-heating systems, sterilization systems, and heat-recovery circuits.
In saturated-steam applications, the meter can support allocation, production monitoring, and utility-cost analysis. In superheated-steam systems, it can help track energy distribution to turbines, process heaters, and high-temperature equipment. When pressure and temperature vary significantly, compensation should be considered so that the reported value reflects the intended volumetric or mass-related calculation.
Steam measurement requires careful attention to condensation. The line should be designed and installed to prevent excessive liquid accumulation, and the meter should be oriented according to the process conditions. Drainage, insulation, upstream and downstream piping, and the selection of gaskets and connection components all affect measurement quality.
Steam Flow Monitoring in Sterilization and SIP Systems
Clean steam is used in pharmaceutical, food, and biotechnology facilities for sterilization-in-place systems, autoclaves, tanks, vessels, and process equipment. The MA80T can support monitoring of clean-steam supply when its materials, surface condition, connection design, and installation meet the applicable hygienic and validation requirements.
Measurement data can be used to verify steam delivery, identify abnormal consumption, support thermal process control, and compare performance between production cycles. The flowmeter should be selected with attention to the cleanliness of wetted materials, the possibility of condensate, the required sterilization temperature, and the plant’s documentation requirements.
Applications in Gas and Compressed-Air Networks
Compressed air is often one of the least visible but most expensive utilities in an industrial plant. Leakage, inappropriate pressure settings, oversized compressors, and uncontrolled demand can significantly increase energy consumption. Installing flowmeters at compressor outlets, production areas, and major branches helps plant personnel identify consumption patterns and abnormal demand.
The MA80T can measure compressed air and other clean utility gases when the flow range, pressure, temperature, and piping configuration are suitable. Its 4–20 mA and pulse outputs can feed a central energy-management platform, while digital communication can support parameter review and diagnostics.
Nitrogen and inert gases are also used in chemical, petrochemical, pharmaceutical, electronics, and food-processing facilities. Flow measurement supports blanketing, purging, process protection, and consumption control. The MA80T can be considered for these applications when the gas is clean and the required operating range is appropriate.
Fuel Gas and Burner Systems
Fuel gas measurement is important for combustion efficiency, burner balancing, process stability, and emission reduction. The MA80T can be installed in fuel-gas lines supplying boilers, furnaces, heaters, and other combustion equipment. The measured flow can be compared with air flow to support air–fuel ratio control and identify changes in burner performance.
Gas pressure and temperature should be considered when calculating standard or mass-equivalent flow. The flowmeter configuration, hazardous-area requirements, electrical installation, and local safety standards must also be reviewed. Where the gas contains liquids, heavy contaminants, or unstable multiphase components, additional conditioning or a different measurement technology may be necessary.
Applications in Liquid Systems
Although vortex meters are commonly associated with steam and gas, the MA80T can also measure clean, low-viscosity, single-phase liquids. Suitable examples may include utility water, condensate, hot water, chilled water, and selected clean process liquids. The application must provide sufficient velocity and stable flow conditions for reliable vortex formation.
In HVAC and district-energy systems, the MA80T can monitor hot-water and chilled-water circulation. Plant operators can use the data to identify imbalance between branches, verify pump performance, assess thermal-energy distribution, and detect changes in demand. For energy calculations, flow measurement may be combined with supply and return temperature data.
In chemical and petrochemical plants, the meter may be used for clean transfer liquids, utility water, or selected low-viscosity process streams. Material selection is important when the medium is corrosive. SS316L, Hastelloy alloys, titanium, or other wetted materials may be considered depending on the chemical composition, concentration, temperature, and pressure.
The MA80T should not be treated as a universal liquid meter. Liquids with high viscosity, entrained gas, suspended solids, severe pulsation, or rapidly changing phase conditions may require electromagnetic, Coriolis, ultrasonic, or another specialized technology. Application review is essential before final selection.
Installation Requirements
Correct installation is necessary to preserve the flow profile required for stable vortex formation. Typical guidance calls for approximately 15 nominal pipe diameters of straight pipe upstream and 5 nominal pipe diameters downstream. The exact requirement depends on the presence of elbows, valves, reducers, expanders, pumps, compressors, regulators, and other disturbances.
The meter should be installed in a section of pipe that remains full for liquid applications. The internal diameter of the connected pipe should match the selected meter and should not introduce abrupt steps or misalignment. Gaskets must be correctly centered so that they do not project into the flow path. Welding residues, scale, and debris should be removed before commissioning.
For gas and steam systems, the installation should minimize liquid accumulation and avoid locations where condensate can collect around the sensor. For high-temperature service, the electronics must remain within their rated ambient-temperature range. If the meter uses a remote converter or extended connection arrangement, the cable routing should be protected from high vibration, strong electromagnetic interference, and excessive heat.
Vibration is a significant consideration for vortex measurement. Pumps, compressors, rotating machinery, unsupported pipework, and pulsating valves can create signals that interfere with vortex detection. The meter should be installed on a mechanically stable pipe section, and nearby equipment should be evaluated during commissioning if signal quality is inconsistent.
Orientation
The MA80T can be installed in horizontal or vertical pipe runs when the system is correctly designed. Orientation should be selected according to the medium, temperature, drainage requirements, and accessibility. For liquid service, a configuration that keeps the pipe full and avoids air pockets is essential. For steam and gas, the orientation should support stable phase conditions and limit condensate-related disturbances.
Sizing
Meter sizing should be based on minimum, normal, and maximum flow rather than line size alone. The selected nominal diameter should provide adequate velocity across the expected operating range while avoiding excessive pressure loss and over-range conditions. For steam and gas, density changes caused by pressure and temperature should be included in the calculation.
Oversizing can reduce the velocity below the meter’s reliable operating range. Undersizing can result in excessive velocity, pressure loss, noise, or a flow rate beyond the instrument’s specified range. VNER’s engineering-driven selection process is intended to help users evaluate these factors before ordering.
Outputs, Communication, and Diagnostics
The standard 4–20 mA output is widely used in industrial control systems because it is resistant to voltage drop and suitable for long cable runs. A pulse output can be used for totalization, batching, or connection to a counter input. These outputs allow the MA80T to be integrated into existing control architectures without major changes.
HART communication provides access to digital configuration and additional process information while retaining the conventional current loop. Modbus RTU can support communication with supervisory systems, remote terminal units, programmable controllers, and energy-management platforms. Communication options should be specified according to the plant’s existing network and instrument-management practices.
Diagnostics may include signal-quality monitoring, sensor fault indication, and basic self-checks. These functions can help maintenance teams distinguish between a genuine process change and a measurement problem. For example, a sudden loss of signal quality may indicate excessive vibration, an unsuitable flow condition, sensor damage, or wiring issues.
Local display options can provide immediate access to flow rate, totalized flow, status, and configuration information. A local display is especially useful during commissioning, routine inspection, and troubleshooting in areas where access to the control room is limited.
Manufacturing Strengths and Quality Control
The performance of an industrial flowmeter depends not only on its measurement principle but also on manufacturing consistency. The geometry of the bluff body, the alignment of the sensor, the quality of the pressure boundary, the electronic assembly, and the calibration process all influence final performance. For this reason, the MA80T is supported by a manufacturing organization that combines product development, production, calibration, and application engineering.
Jiangsu Vner Electronic Technology Co., Ltd. operates modern facilities across three plants, with approximately 23,000 square meters of production and technical space. Its team includes more than 150 technical personnel. Since 2011, the company has focused on industrial flow measurement and has delivered more than 2,000 engineering projects in over 30 countries.
The company’s production approach emphasizes repeatability, traceability, and process control. Manufacturing activities may include material verification, body machining or fabrication, sensor assembly, electronics integration, pressure testing, output verification, calibration, and final inspection. Each stage contributes to the reliability of the completed instrument.
In-House Calibration
Calibration is a critical step in flowmeter production. It verifies that the meter responds correctly over defined operating points and that the output corresponds to the expected flow value. In-house calibration allows the manufacturer to control testing conditions, review results, identify deviations, and maintain records linked to the product.
For a vortex meter, calibration and verification can help confirm sensor response, signal processing, output scaling, and the relationship between measured frequency and flow. Calibration requirements may vary according to medium, nominal diameter, accuracy class, customer specification, and application. Documentation can be supplied according to the project requirements.
Material and Construction Options
Different industrial media require different wetted materials. SS304 may be suitable for many general utility applications, while SS316L may be selected for improved corrosion resistance. Hastelloy alloys and titanium can be considered for more demanding chemical environments when compatible with the process conditions.
Material selection should consider not only the primary fluid but also cleaning chemicals, concentration, temperature, pressure, erosion risk, and possible contamination. The availability of multiple sensor and body material options enables the MA80T to be configured for a wider range of industrial duties than a fixed-material instrument.
Engineering Support and Product Selection
Flowmeter selection involves more than identifying the pipe diameter. Engineers need to review the medium, minimum and maximum flow, operating pressure, operating temperature, density, viscosity, allowable pressure loss, connection standard, area classification, output requirements, and installation conditions.
VNER supports EPC contractors, end users, and OEM partners with sizing and selection assistance. Its portfolio of multiple measurement technologies provides an additional advantage: if a vortex meter is not suitable because of multiphase flow, high viscosity, low conductivity, or another limitation, another measurement principle can be considered within the same engineering supply network.
Benefits for Different Industries
Power and Energy
Power plants and energy facilities use steam, condensate, cooling water, fuel gas, and compressed air throughout their operations. The MA80T can support boiler monitoring, turbine auxiliary systems, heat recovery, steam allocation, condensate-return tracking, and combustion optimization. Reliable utility measurement helps operators identify losses and compare actual consumption with production targets.
Oil and Gas
Oil and gas facilities require measurement of fuel gas, natural gas, steam, utility air, nitrogen, and process support fluids. The MA80T can be applied to non-custody-transfer utility and process services where its pressure, temperature, accuracy, and material specifications are appropriate. Installation design should consider hazardous areas, gas composition, pressure variation, and the possibility of liquid carryover.
Chemical and Petrochemical
Chemical plants often operate extensive networks of steam, nitrogen, compressed air, cooling water, and clean process liquids. The availability of stainless-steel and optional alloy sensor materials allows the MA80T to be considered for a range of chemical services. The process medium must be reviewed carefully to ensure that the selected materials and measurement principle are suitable.
Food and Beverage
Food and beverage plants use clean steam, carbon dioxide, compressed air, hot water, chilled water, and cleaning utilities. The MA80T can support utility monitoring and clean-steam measurement where the construction and installation meet the facility’s hygienic requirements. Accurate utility data can support production costing, energy reduction, sterilization control, and maintenance planning.
Pharmaceutical Manufacturing
Pharmaceutical facilities use clean steam in sterilization-in-place systems and autoclaves, as well as compressed gases and temperature-controlled water loops. The MA80T may be applied when its materials, surface condition, connection design, and documentation satisfy the project’s validation and compliance requirements. Measurement data can assist with process verification and utility qualification.
Textile and Dyeing
Textile plants consume large quantities of process steam, hot water, utility water, and compressed air. Flowmeters installed on dyeing, drying, finishing, and boiler lines can help track consumption, identify abnormal demand, and improve energy allocation. The MA80T is suitable for steam and selected clean utility liquids within its operating limits.
Pulp and Paper
Pulp and paper facilities use steam for drying, condensate for recovery, and compressed air for instrumentation and process equipment. The MA80T can support steam-delivery monitoring and condensate-recovery management where the medium remains within the applicable single-phase and material limits.
Maintenance and Long-Term Operation
The MA80T’s no-moving-parts design reduces routine mechanical maintenance. Nevertheless, periodic inspection remains important. Operators should review process values, output stability, diagnostic status, flange condition, wiring integrity, and the presence of external vibration. The meter should be checked against expected production or utility data to identify gradual changes.
If the application involves dirty gas, wet steam, or contaminated liquids, the upstream piping and process condition should be inspected. Deposits or foreign material around the bluff body can alter the effective flow geometry and affect signal quality. The meter should be isolated and inspected only in accordance with the plant’s safety procedures.
Electrical maintenance should include checking cable glands, grounding, terminal connections, communication settings, and environmental sealing. High humidity, chemical vapors, temperature cycling, and vibration can affect field wiring even when the flowmeter itself remains mechanically sound.
Recalibration intervals depend on the application, regulatory requirements, quality system, and criticality of the measurement. Utility monitoring may use a different interval from a validated pharmaceutical process or a high-value process-control application. Maintaining calibration records supports traceability and helps establish confidence in long-term performance.
How to Select the Correct MA80T Configuration
The first step is to define the medium accurately. The selection process should identify whether the service is saturated steam, superheated steam, compressed air, natural gas, nitrogen, condensate, water, or another clean fluid. For gases and steam, pressure and temperature ranges are essential because density and volumetric flow can change significantly.
The second step is to provide minimum, normal, and maximum flow rates. If only a nominal flow rate is available, the resulting selection may not cover startup, turndown, or peak demand. The line size, upstream and downstream piping, valve arrangement, and available straight length should also be provided.
The third step is to determine material and connection requirements. SS304, SS316L, Hastelloy, titanium, flanged connections, wafer connections, and applicable GB, DIN, or ANSI standards may be selected according to the system design. Pressure class, gasket type, temperature rating, and hazardous-area requirements should be reviewed as part of the complete package.
The fourth step is to define the output and communication requirements. A basic installation may require only a 4–20 mA output and pulse totalization. A larger plant may require HART, Modbus RTU, remote diagnostics, local display, or integration with an energy-management network.
Finally, the installation environment should be evaluated. Ambient temperature, vibration, electromagnetic interference, accessibility, pipe orientation, insulation, and drainage can all affect performance. Providing complete application information allows the manufacturer to recommend the most suitable model and avoid costly changes after delivery.
Frequently Asked Questions
What media can the MA80T measure?
The MA80T is designed for saturated steam, superheated steam, gases, and clean or low-viscosity single-phase liquids. Typical examples include compressed air, nitrogen, inert gas, natural gas, fuel gas, utility water, condensate, hot water, chilled water, and selected clean process liquids.
Does the MA80T measure mass flow directly?
The MA80T primarily measures volumetric flow through vortex frequency. For steam and gases, pressure and temperature compensation may be used to calculate standardized or mass-related values when the system is configured appropriately. Applications requiring direct mass measurement and density information may be better suited to Coriolis technology.
Does the meter have moving parts?
No. The MA80T uses a fixed bluff body and piezoelectric sensor. The absence of rotating or sliding components reduces mechanical wear and helps lower routine maintenance requirements.
What accuracy can be expected?
Typical liquid accuracy can reach up to ±1.0% of rate under calibrated conditions. Typical gas and steam accuracy is approximately ±1.0% to ±1.5% of rate. Actual performance depends on model, sizing, medium, flow range, piping, installation, and calibration conditions.
How much straight pipe is required?
A typical guideline is approximately 15 nominal pipe diameters upstream and 5 nominal pipe diameters downstream. The final requirement should be confirmed according to the installation arrangement and the disturbances created by elbows, valves, reducers, pumps, compressors, or regulators.
Can the MA80T be installed in a vertical pipe?
Yes, horizontal and vertical installation can be supported when the meter is correctly sized and installed. The preferred orientation depends on the medium, drainage, phase stability, temperature, and accessibility.
Is the MA80T suitable for compressed air?
Yes. Compressed-air monitoring is a common application when the flow range, pressure, temperature, gas cleanliness, and piping conditions are suitable. The output can be connected to a control system or energy-management platform to monitor consumption and identify leakage or abnormal demand.
Can it measure high-temperature steam?
Standard versions can operate up to approximately 250 °C, while high-temperature versions can reach approximately 350 °C. The exact temperature limit depends on the selected model and complete installation configuration.
Which communication options are available?
Available options include 4–20 mA, pulse, HART, and Modbus RTU. The suitable combination depends on the control architecture and the required diagnostic or remote-configuration functions.
How should the meter be sized?
Sizing should use minimum, normal, and maximum flow values together with pressure, temperature, density, viscosity, line size, and allowable pressure loss. Selecting only by pipe diameter can cause poor low-flow performance or excessive velocity at peak flow.
Can the MA80T measure dirty or multiphase fluids?
The MA80T is intended mainly for clean, single-phase media. Significant solids, entrained gas, wet steam, pulsation, or multiphase flow may affect vortex formation and signal stability. Such applications require detailed review and may need another flowmeter technology or upstream conditioning.
What materials are available?
Body and flange materials include SS304 and SS316L. Depending on the model, wetted sensor materials may include SS304, SS316L, Hastelloy C, Hastelloy B, and titanium. Material selection should be based on the actual process chemistry and operating conditions.
Why choose a vortex meter instead of a turbine meter?
A vortex meter has no rotor, bearings, or gears, so it can reduce mechanical wear and maintenance. It is also well suited to steam and many gas applications. A turbine meter may still be advantageous for certain clean-liquid duties or specialized low-flow applications, so the choice should be based on process requirements rather than technology alone.
Conclusion
The MA80T Series Vortex Flowmeter provides a balanced solution for industrial measurement of steam, gases, and clean liquids. Its Kármán vortex principle, piezoelectric detection, fixed bluff body, and lack of moving parts support stable operation with reduced mechanical maintenance. Flanged and wafer configurations, multiple materials, high-temperature options, practical accuracy, and industrial communication interfaces make the series adaptable to utility and process applications.
The meter is especially valuable for steam distribution, compressed-air monitoring, fuel-gas measurement, burner optimization, HVAC loops, district energy, clean-steam systems, and utility-water management. Compared with turbine, electromagnetic, Coriolis, thermal mass, and ultrasonic technologies, it offers a distinctive combination of broad medium compatibility, industrial robustness, and cost-conscious operation.
Its performance depends on correct engineering selection and installation. Minimum and maximum flow, pressure, temperature, fluid condition, straight-run piping, vibration, material compatibility, and communication requirements should all be reviewed before purchase. Supported by in-house calibration, controlled manufacturing, a broad technology portfolio, and international project experience, Jiangsu Vner Electronic Technology Co., Ltd. provides more than an individual instrument. It offers application-oriented flow measurement support for EPC contractors, plant operators, OEMs, and industrial users seeking dependable long-term measurement.
References
1. International Organization for Standardization. Measurement of Fluid Flow in Closed Conduits: General Principles of Flow Measurement.
2. International Organization for Standardization. Measurement of Fluid Flow in Closed Conduits Using Velocity-Measuring Devices.
3. American Society of Mechanical Engineers. Measurement of Fluid Flow in Pipes Using the Devices and Installation Requirements for Vortex Flowmeters.
4. International Electrotechnical Commission. Industrial-Process Measurement and Control Equipment: Electromagnetic Compatibility Requirements.
5. International Society of Automation. Industrial Process Measurement and Control: Flow Measurement Principles and Applications.
6. Instrumentation and Automation Engineering References. Vortex Shedding, Strouhal Relationships, and Industrial Flowmeter Installation Practice.
7. Jiangsu Vner Electronic Technology Co., Ltd. MA80T Series Vortex Flowmeter Product and Application Information.
Product: MA80T Series Vortex Flowmeter
Products
Contact Information
-

+86 18652789521
+86-0514-83633600 / 83633900 -

+86-0514-83633600 / 83633900
-

s@vner.com.cn
katherine@vner.com.cn -

No. 11 Xingye Road, Chenji Town Industrial Park, Yizheng, Yangzhou, China
