 0
 EN
 English
 عربى
 Español
 русский
If you need any help, please feel free to contact us
Home / Author / Guo Lanyue — Industrial Flow Meter Sales Manager / Industrial Swirl Flowmeters for Accurate Liquid, Gas, and Steam Measurement
Industrial Swirl Flowmeters for Accurate Liquid, Gas, and Steam Measurement
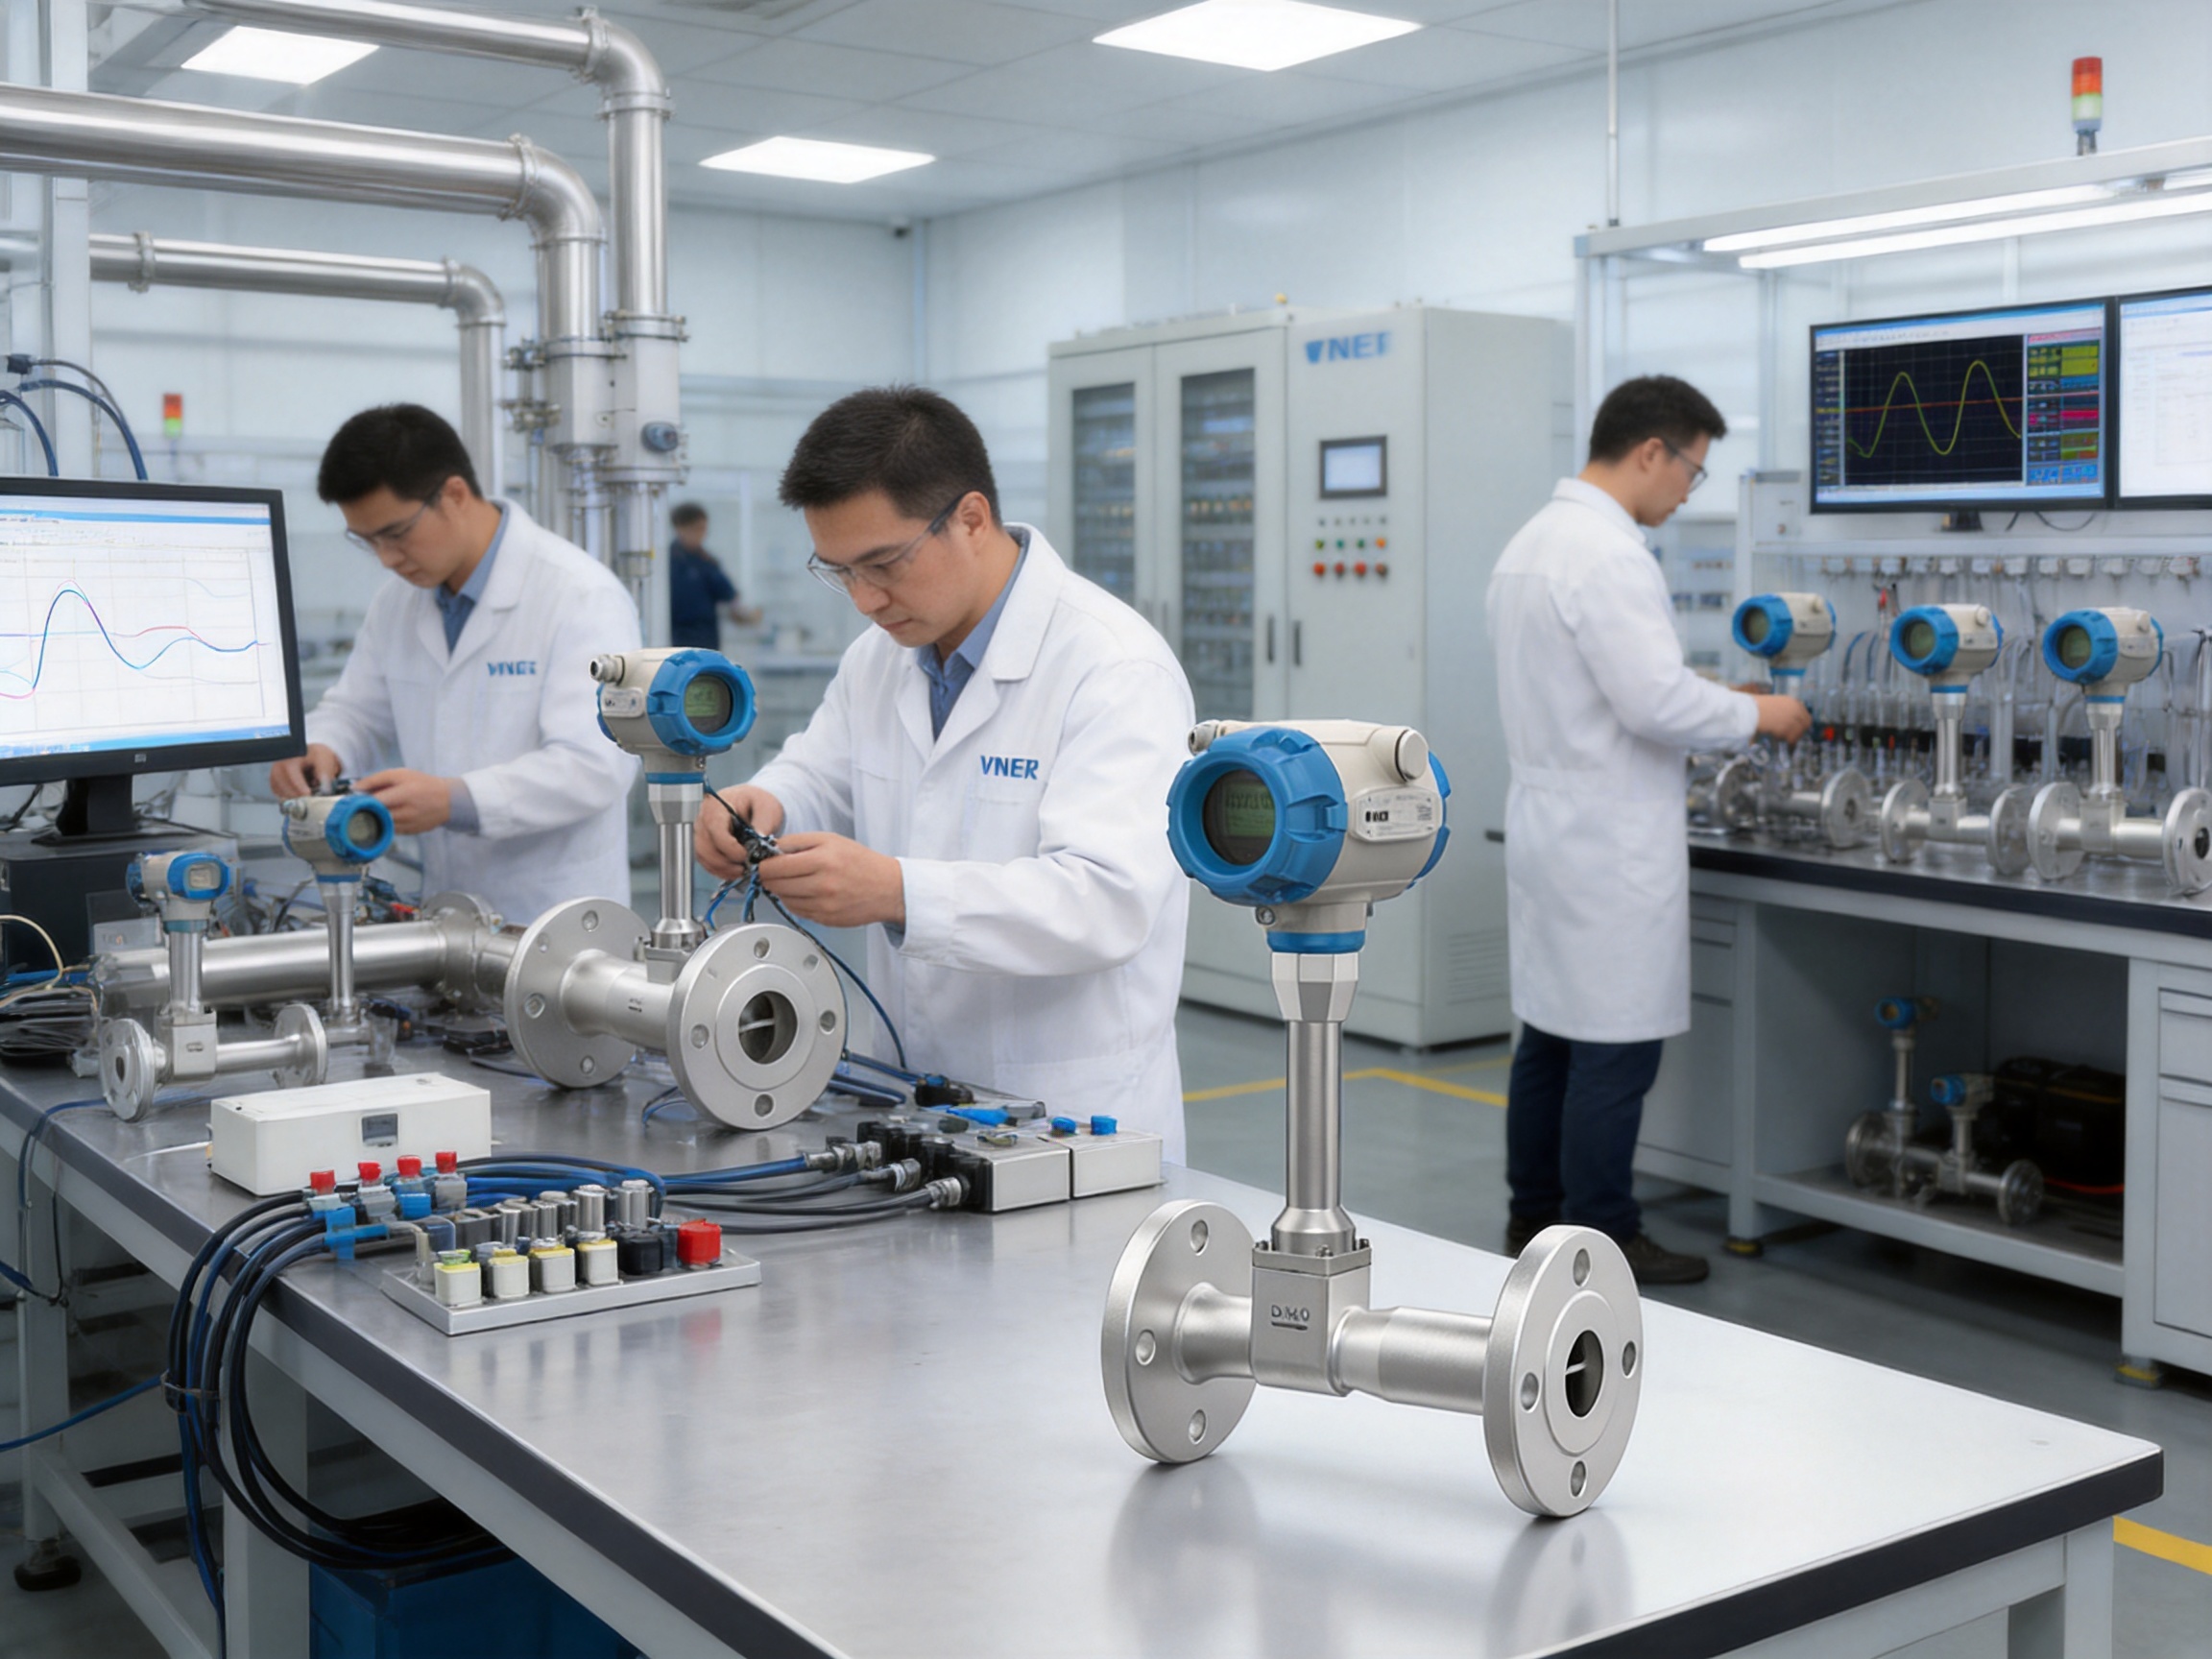
Reliable flow measurement is essential to modern process industries. Whether a plant is monitoring boiler steam, controlling compressed air, regulating chemical reactants, measuring cooling water, or managing process gas, the flowmeter must deliver stable readings under changing temperature, pressure, and operating conditions. A measurement error can affect product quality, energy consumption, equipment safety, production efficiency, and regulatory compliance. For this reason, industrial users increasingly require instruments that combine accuracy, durability, broad application coverage, simple maintenance, and flexible communication capabilities.
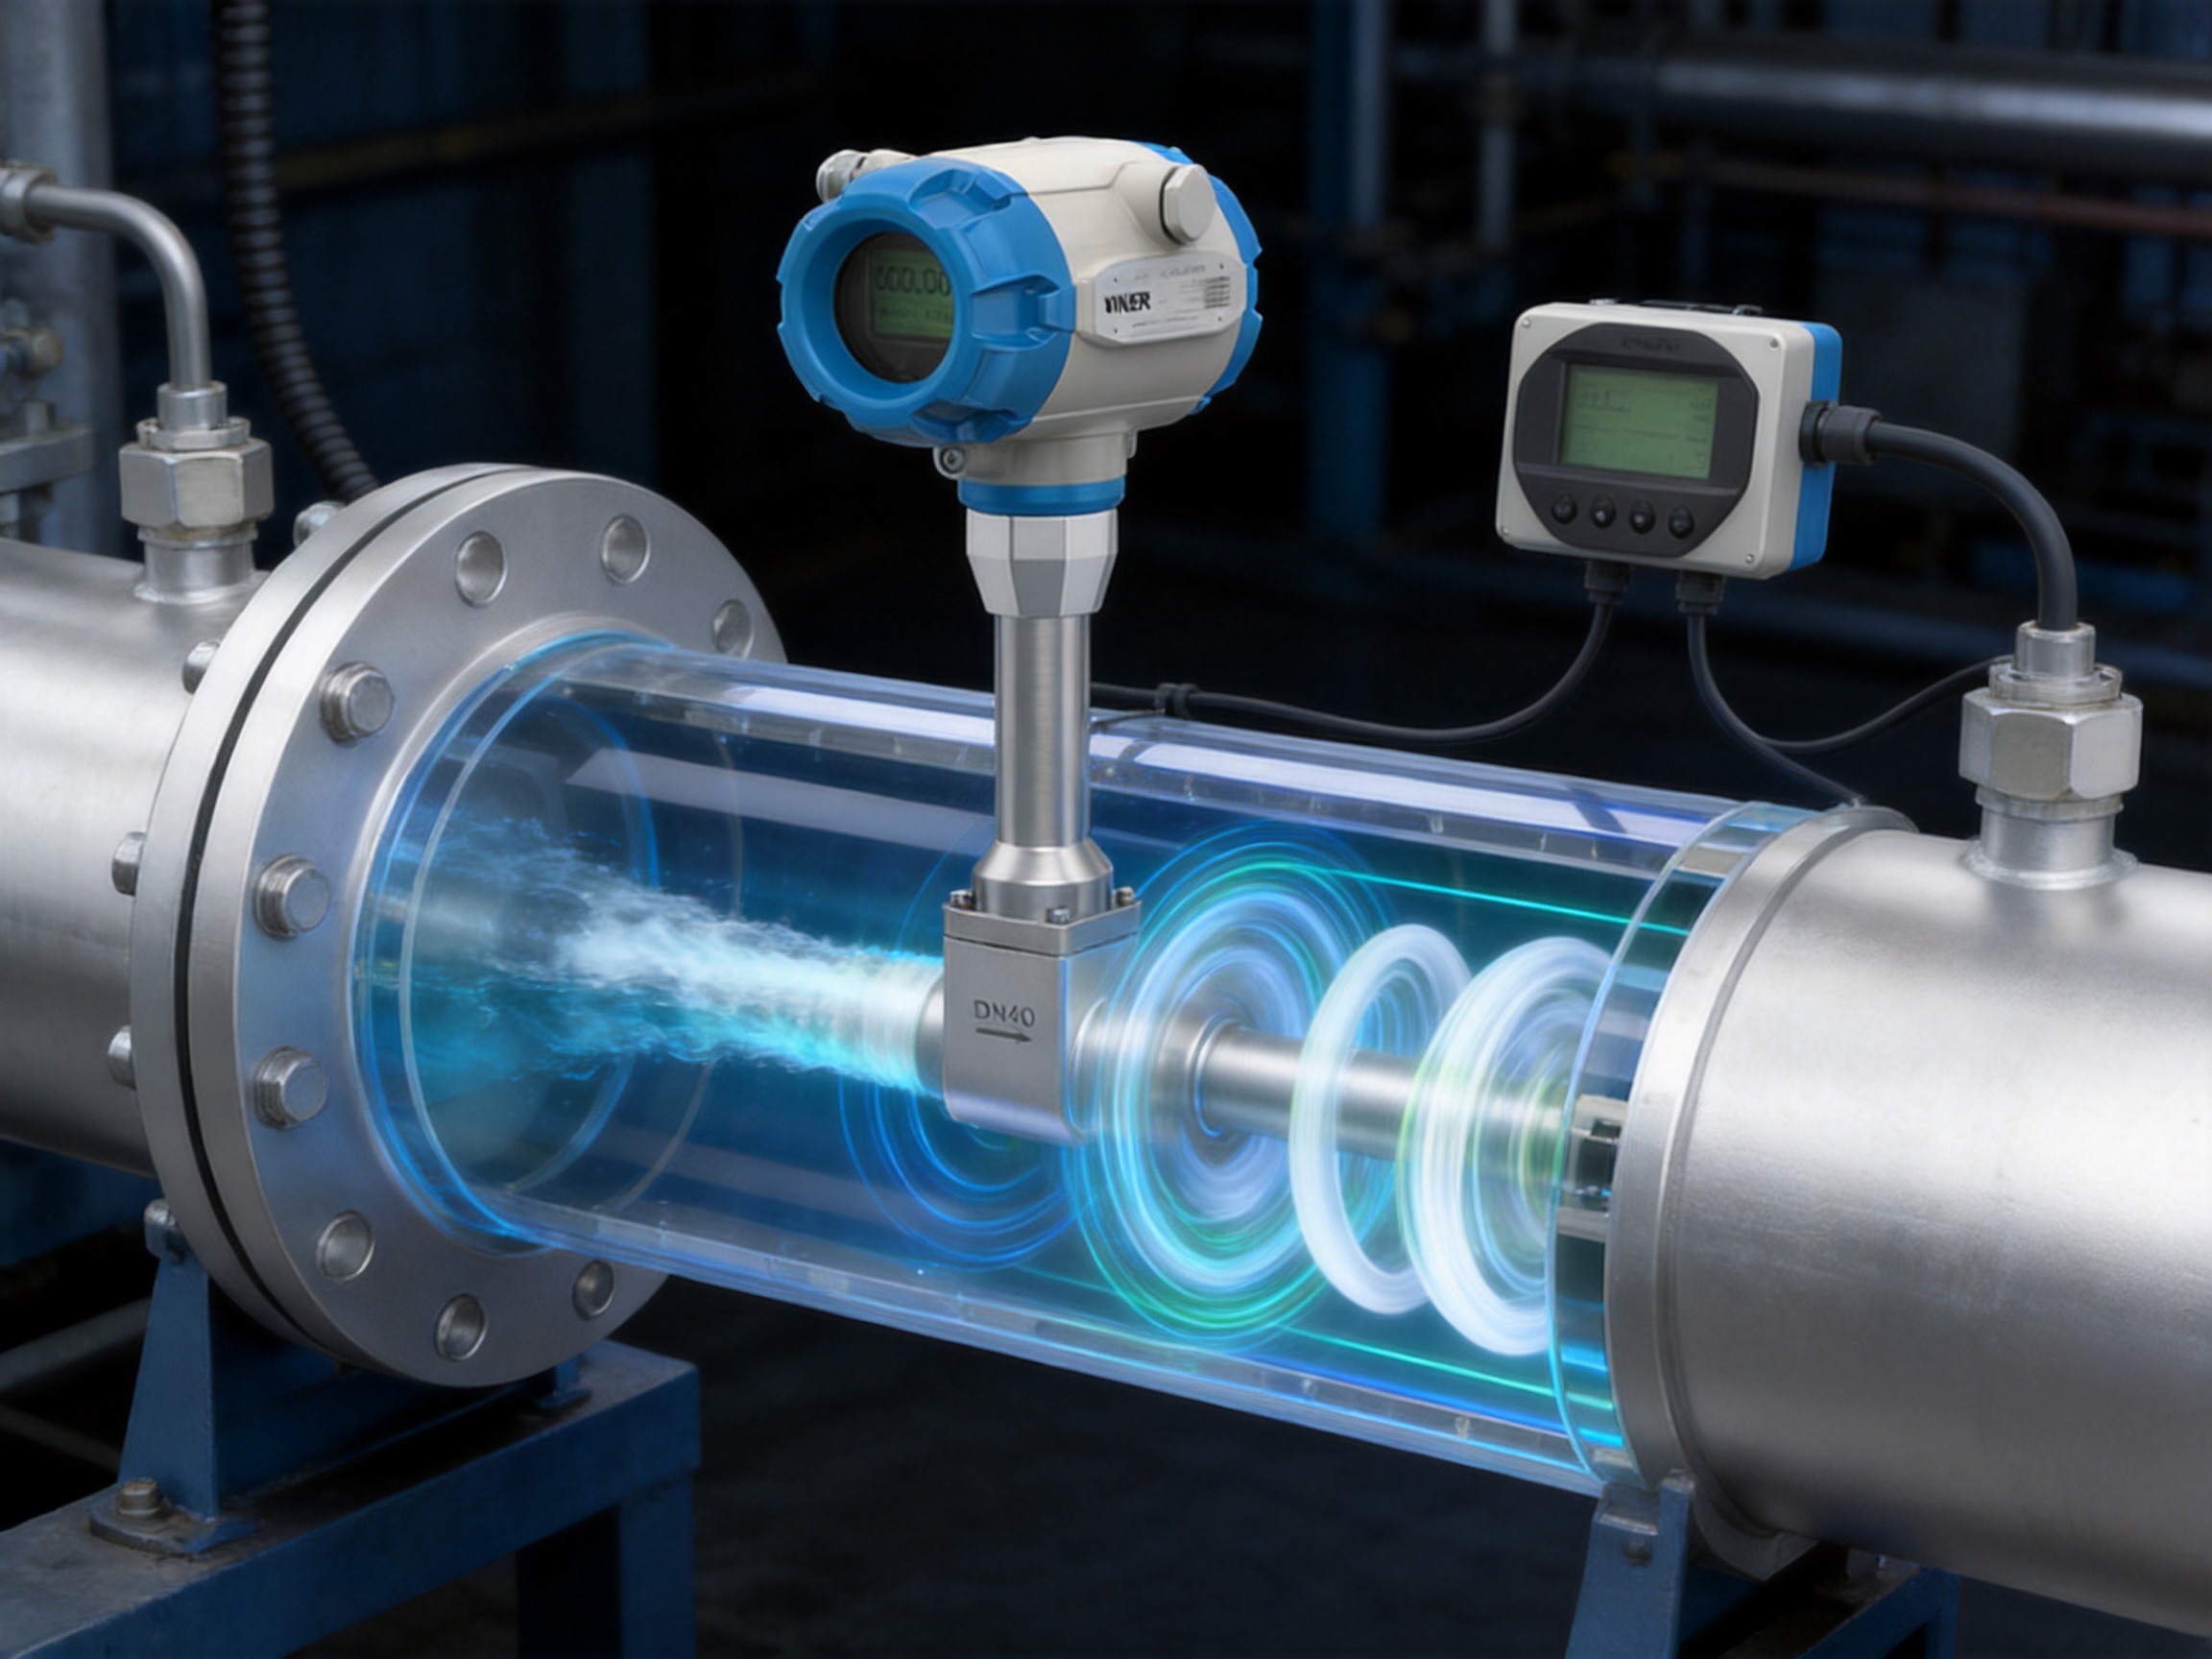
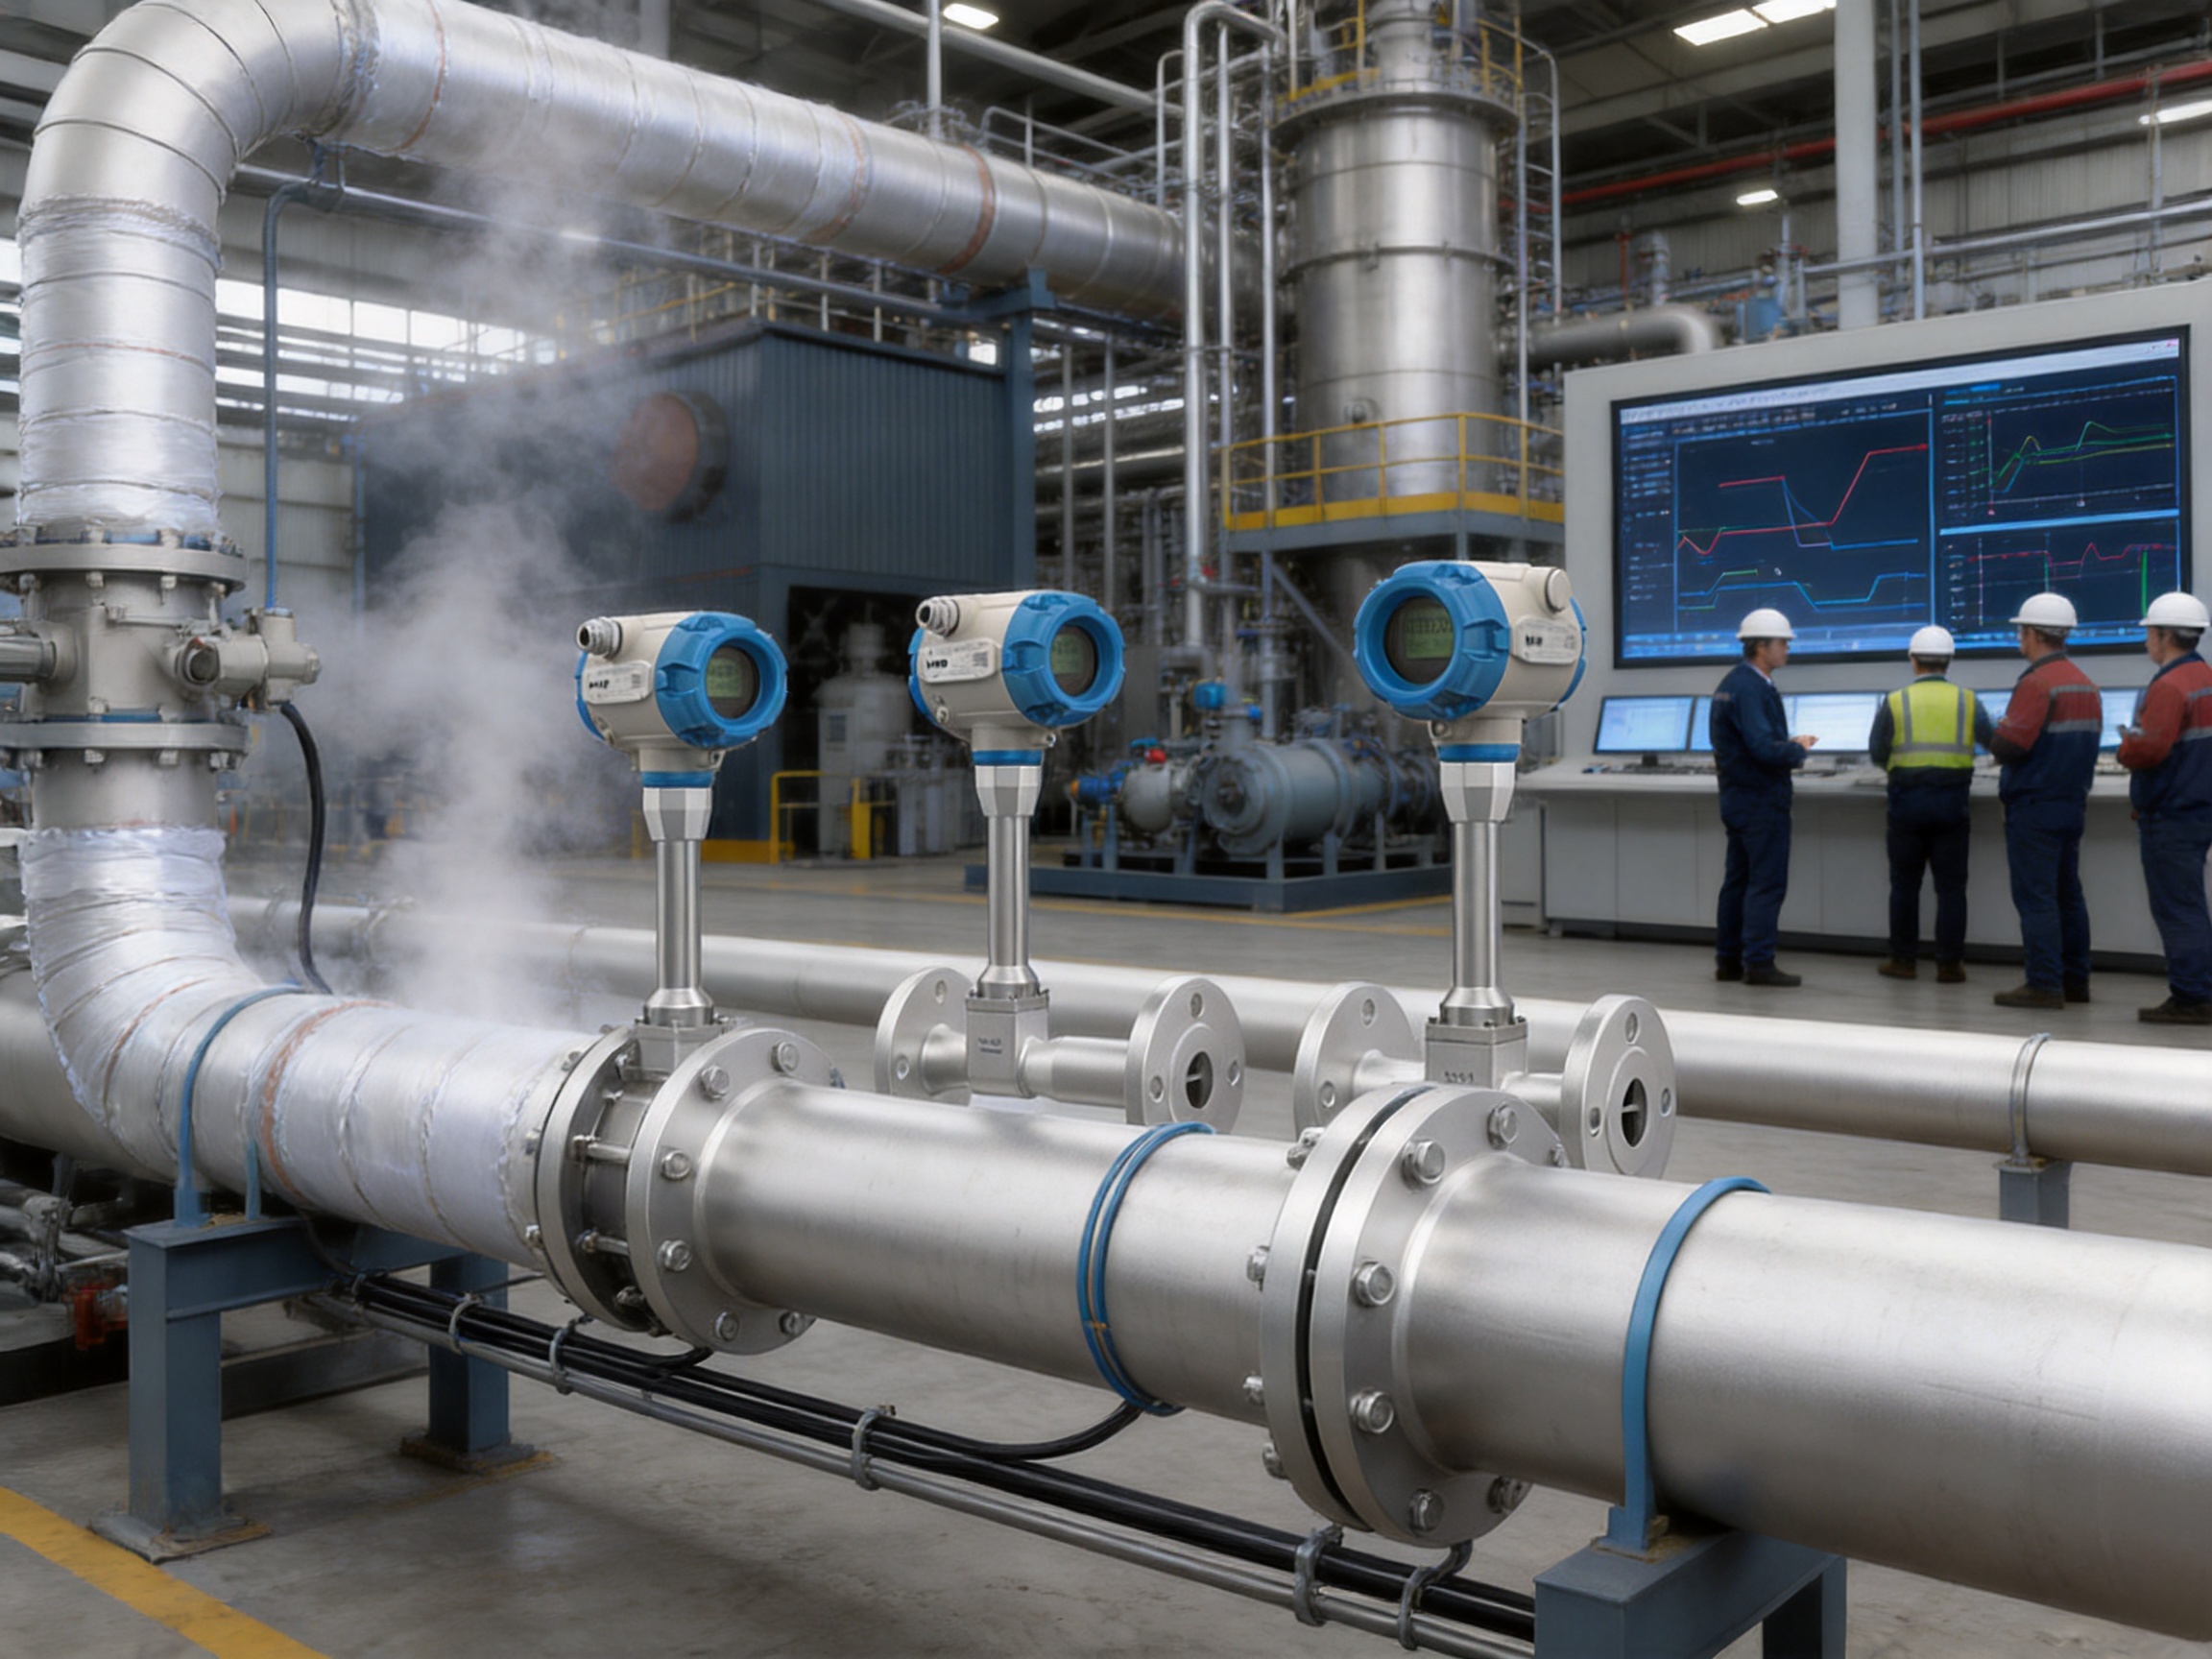
The SA80T Series Swirl Flowmeter is designed to meet these requirements. It is a vortex precession flowmeter for measuring liquids, gases, and saturated or superheated steam. Its sensing principle is based on the formation of a controlled swirling flow inside the meter body. As the process medium passes through a fixed swirl generator, the fluid is forced into a rotating motion. A stable vortex precession develops downstream, and its frequency is directly proportional to the volumetric flow rate.
The precession signal is detected by a non-intrusive piezoelectric sensor. Because the sensor does not extend into the process stream and does not rely on moving mechanical components, the meter can operate reliably in demanding industrial environments. The design is suitable for clean and slightly contaminated media and can be configured for a wide range of liquid, gas, and steam applications.
Manufactured by Jiangsu Vner Electronic Technology Co., Ltd., the SA80T Series reflects an engineering approach that combines process measurement expertise, in-house calibration, digital signal processing, industrial manufacturing, and application-oriented product selection. The company provides flow measurement solutions for liquid, gas, and slurry services and supports industrial customers, engineering contractors, original equipment manufacturers, and system integrators in multiple countries.
Understanding the Swirl Flow Measurement Principle
Swirl flow measurement is based on a controlled vortex generated inside the flow passage. Unlike a conventional turbine meter, the instrument does not depend on a rotor turning in the fluid. Unlike a traditional differential pressure meter, it does not require a pressure-tapping system to calculate flow from a permanent restriction. Instead, the SA80T uses a fixed internal structure to create a rotating flow pattern and then measures the frequency of the resulting vortex precession.
When the process fluid enters the flow body, the swirl generator redirects part of the axial flow into a rotational pattern. The fluid then forms a vortex whose axis moves in a controlled precessional path. This movement produces a repeatable pressure fluctuation. The frequency of this fluctuation increases as the volumetric flow rate increases. By processing the frequency signal, the transmitter calculates the flow rate and provides a corresponding output.
The relationship between vortex frequency and flow is highly repeatable within the operating range. This enables the meter to provide real-time measurement without mechanical wear caused by rotating parts. Since the piezoelectric sensor is non-intrusive, it is isolated from direct contact with the process medium. This feature is especially valuable when the fluid is hot, pressurized, chemically aggressive, or unsuitable for direct contact with a conventional mechanical sensor.
The output can be used for volumetric flow measurement or, when suitable temperature and pressure compensation is available, for standard volume or mass-related process calculations. This makes the SA80T suitable not only for local indication but also for plant control systems, energy management platforms, distributed control systems, supervisory control and data acquisition systems, and production monitoring networks.
Core Product Characteristics
Accurate Measurement Across Multiple Media
The SA80T Series is designed to measure liquids, gases, saturated steam, and superheated steam. Under calibrated conditions, typical accuracy can reach approximately ±0.5% for liquids and ±1.0% for gases and steam. Actual performance depends on meter size, fluid properties, Reynolds number, installation quality, calibration conditions, and the selected measurement range.
This level of performance supports applications in which flow data is used for process control, utility allocation, energy optimization, batch monitoring, and equipment protection. The meter can help operators identify abnormal consumption, verify process recipes, monitor boiler output, and regulate the flow of gases or liquids in response to changing production requirements.
Wide Turndown Capability
The flowmeter can provide a turndown ratio of up to 1:20, depending on the measured medium and installation conditions. A wide turndown ratio is important when the process does not operate at a single fixed load. Many industrial systems experience seasonal variations, production changes, startup and shutdown periods, or intermittent demand from multiple users.
A meter with insufficient range may become inaccurate or unstable at low flow, while a meter selected only for peak flow may be oversized for normal operation. The SA80T helps reduce this compromise by maintaining useful measurement performance over a broad operating window. Correct sizing remains essential, and the final selection should consider minimum flow, normal flow, maximum flow, pressure, temperature, density, viscosity, and the required output signal.
No Moving Parts
A major advantage of the SA80T design is the absence of moving mechanical components in the flow measurement mechanism. Turbine meters use rotating blades or rotors that can wear, become fouled, or require inspection. Mechanical displacement meters may contain gears, pistons, or other components that are sensitive to contamination and lubrication conditions. The fixed swirl generator and piezoelectric sensing principle avoid these common maintenance concerns.
The absence of moving parts contributes to long service life and consistent performance. It also reduces the likelihood of mechanical failure caused by bearing wear, shaft damage, rotor imbalance, or changes in friction. This makes the flowmeter suitable for continuous process operation where planned maintenance opportunities are limited.
Non-Intrusive Piezoelectric Sensing
The piezoelectric sensor detects the pressure fluctuation associated with vortex precession without direct contact with the flowing medium. This arrangement separates the sensitive signal-detection element from the process stream. It helps protect the sensor from high-temperature media, process chemicals, and normal flow contamination.
Non-intrusive detection also supports a compact internal structure. With no probe or rotating assembly extending deeply into the flow path, the meter can maintain a robust and relatively simple construction. The design is suitable for industrial environments in which reliability and minimal maintenance are more important than frequent mechanical adjustment.
Integrated Signal Processing
The transmitter processes the sensor signal and converts the precession frequency into a useful flow measurement. Depending on the configuration, available outputs include 4–20 mA analog output, pulse output, HART communication, and Modbus RTU communication. This allows the instrument to interface with both conventional control loops and modern digital plant networks.
Optional temperature and pressure compensation can support standard volume flow or mass-related calculations for gases and steam. Compensation is particularly important because gas and steam density changes substantially with operating pressure and temperature. Without compensation, a volumetric reading at process conditions may not accurately represent the actual quantity of gas or steam used by the plant.
Self-Diagnostics and Smart Configuration
Modern industrial measurement equipment must do more than display a number. It should also help operators understand whether the measurement is valid. The SA80T supports functions such as fault detection, zero-drift monitoring, and remote configuration through digital communication protocols, depending on the selected model and transmitter configuration.
Diagnostic functions can help identify abnormal signal conditions, incorrect configuration, wiring problems, or process conditions outside the expected range. Remote configuration reduces the need to open an enclosure or access a difficult installation point. In large plants, this can improve maintenance efficiency and reduce the time required for commissioning or troubleshooting.
High Temperature and Pressure Resistance
Standard designs support temperatures up to approximately 250°C and pressures up to approximately 4.0 MPa. Extended versions can be configured for higher-temperature steam service, with options reaching approximately 400°C. These capabilities make the series suitable for boiler systems, thermal oil facilities, process heating networks, steam distribution pipelines, and other high-energy applications.
High-temperature and high-pressure service places demanding requirements on the body, seals, sensor arrangement, electronics, insulation, and installation accessories. The complete instrument configuration must be selected according to the process conditions. Users should provide accurate design pressure, operating pressure, design temperature, operating temperature, fluid composition, and ambient conditions when requesting a quotation or technical selection.
Advantages Compared with Conventional Flowmeter Technologies
Comparison with Turbine Flowmeters
Turbine flowmeters can provide good accuracy for clean liquids and gases, but their rotating components are vulnerable to wear and contamination. Particles, droplets, viscous materials, or sudden hydraulic disturbances may affect the rotor. Over time, bearing friction and mechanical wear can change the relationship between flow and output.
The SA80T does not use a rotating rotor. Its fixed swirl generator and piezoelectric sensor reduce mechanical wear and eliminate the need to maintain bearings or moving shafts. This is a valuable advantage in continuous-duty systems, especially where the process medium is not perfectly clean or where maintenance access is restricted.
Comparison with Differential Pressure Meters
Orifice plates, venturi tubes, and other differential pressure devices determine flow from a pressure difference across a restriction. These systems are widely used, but they may introduce permanent pressure loss, require impulse lines, and demand careful maintenance in services where lines can plug or freeze. The square-root relationship between differential pressure and flow can also limit low-flow sensitivity.
The SA80T measures vortex frequency instead of relying on a permanent pressure restriction. This can reduce energy loss associated with the primary element and simplify the installation compared with systems requiring separate pressure transmitters and impulse tubing. The actual pressure drop depends on the meter design and operating conditions, but the operating principle avoids the traditional orifice-plate arrangement.
Comparison with Traditional Vortex Meters
Traditional vortex meters commonly use a bluff body to generate alternating vortices. They are widely used for gas, liquid, and steam measurement, but they may require longer straight pipe runs and can be sensitive to certain upstream disturbances. In some installations, space limitations make these requirements difficult to meet.
The SA80T uses a swirl flow principle and can typically operate with minimum upstream and downstream straight pipe requirements of approximately 3D and 1D, subject to the selected model and installation conditions. This can provide a practical advantage in compact piping layouts, skid systems, utility rooms, and retrofit projects where available straight pipe length is limited.
Comparison with Electromagnetic Flowmeters
Electromagnetic flowmeters are excellent for conductive liquids, including many water-based and process-liquid applications. However, they cannot measure non-conductive liquids, gases, or steam. They also require a full pipe and can be affected by installation grounding and conductivity conditions.
The SA80T expands application coverage beyond conductive liquids. It can measure gases and steam as well as liquids, allowing one product family to support multiple utility and process services. This is useful for industrial groups that prefer to standardize procurement, instrumentation training, spare parts, and maintenance procedures across different measurement points.
Comparison with Coriolis Mass Flowmeters
Coriolis meters provide direct mass flow measurement and excellent accuracy, but they can be more expensive and heavier than other flowmeter technologies. Their cost and mechanical configuration may not be necessary for every utility or process application.
The SA80T offers a practical alternative where volumetric flow measurement, compensated gas or steam measurement, or process monitoring is sufficient. It can provide a lower-complexity solution for large line sizes, steam utilities, compressed air, cooling water, and general industrial flow control. For applications requiring direct mass measurement of high-value fluids or very precise batching, Coriolis technology may remain preferable. The correct choice depends on the process objective rather than on accuracy alone.
Product Performance and Selection Considerations
Correct selection is the foundation of good flowmeter performance. The same nominal pipe size can operate under very different conditions depending on fluid density, pressure, temperature, viscosity, and flow range. Before selecting the SA80T, users should provide the following information:
1. Measured medium and chemical composition.
2. Minimum, normal, and maximum flow rate.
3. Operating pressure and design pressure.
4. Operating temperature and design temperature.
5. Fluid density, viscosity, and compressibility where applicable.
6. Pipe material, nominal diameter, and connection standard.
7. Required accuracy and output signal.
8. Whether temperature and pressure compensation is required.
9. Environmental conditions, including ambient temperature, vibration, humidity, and hazardous-area requirements.
10. Available straight pipe length upstream and downstream of the meter.
The following table summarizes common application considerations for different media.
| Medium | Typical Applications | Important Selection Factors | Recommended Functional Options |
|---|---|---|---|
| Liquid | Process water, cooling water, chemical reactants, thermal fluids | Density, viscosity, minimum flow, contamination, pipe filling | Analog output, pulse output, local display, remote communication |
| Compressed air | Factory utilities, pneumatic equipment, instrument air | Pressure, temperature, standard volume reference, leakage monitoring | Pressure and temperature compensation, Modbus or HART |
| Natural gas | Furnaces, boilers, process heaters, gas distribution | Gas composition, pressure, temperature, hazardous-area classification | Compensated flow calculation, pulse and 4–20 mA outputs |
| Saturated steam | Boilers, sterilization, heating systems, process utilities | Steam quality, pressure, temperature, condensate management | Temperature and pressure compensation, high-temperature configuration |
| Superheated steam | Power generation, turbines, process heating | High temperature, high pressure, thermal expansion, insulation | Extended-temperature design, compensated output, remote display |
| Nitrogen, oxygen, or hydrogen | Reactors, inerting, semiconductor and chemical processes | Gas properties, cleanliness, pressure stability, safety requirements | Digital communication, diagnostic functions, suitable material selection |
Installation and Piping Guidance
Even a high-quality flowmeter can deliver poor results if it is installed incorrectly. The SA80T should be installed in a pipe section that remains full when measuring liquids. The pipe should be properly supported, and excessive vibration should be avoided. Valves, reducers, elbows, pumps, compressors, and other disturbances should be positioned according to the recommended installation layout.
The typical straight pipe requirement is approximately 3D upstream and 1D downstream, where D represents the internal pipe diameter. The actual requirements can vary according to the piping arrangement, meter size, flow condition, and manufacturer guidance. Although the SA80T generally requires less straight pipe than many conventional vortex meters, users should not assume that no installation control is necessary.
For liquid measurement, the installation should prevent gas pockets from accumulating around the sensor. If the process contains suspended solids or intermittent bubbles, the piping arrangement should be reviewed carefully. For steam and gas measurement, the pipeline should be designed to minimize condensate accumulation, and suitable drainage or separation equipment should be considered where necessary.
The meter should be oriented according to the process medium and temperature. High-temperature applications may require remote electronics, extended necks, thermal insulation practices, or other protective arrangements. Insulation should not cover components that must dissipate heat unless the approved installation design specifically permits it.
Electrical wiring should be separated from high-power cables and strong electromagnetic interference sources where practical. The signal cable, grounding arrangement, power supply, and communication wiring should follow the applicable instrument and site standards. Before commissioning, the operator should verify the flow direction, nominal diameter, range settings, unit settings, pulse scaling, alarm parameters, and compensation inputs.
Applications in Power Generation and Steam Systems
Steam measurement is one of the most important applications for industrial swirl flowmeters. In a power plant or industrial boiler house, reliable steam data supports combustion optimization, energy allocation, equipment diagnostics, and production planning. The SA80T can be used to monitor saturated steam leaving boilers, superheated steam supplied to process users, and auxiliary steam used in heating or deaeration systems.
In boiler efficiency programs, continuous steam flow data can be combined with fuel consumption, feedwater flow, flue gas information, and pressure and temperature measurements. This allows plant engineers to evaluate the relationship between fuel input and useful steam output. Abnormal changes may indicate burner problems, heat-transfer degradation, steam leakage, or an inaccurate control setting.
Steam flow measurement is also important in thermal processing. Food plants, pharmaceutical facilities, chemical factories, textile plants, and paper mills often use steam for heating, drying, sterilization, or temperature control. Accurate measurement helps departments understand utility consumption and supports fair internal cost allocation.
Cooling water circulation is another application in power generation. Flowmeters can monitor water through turbine auxiliaries, heat exchangers, condensers, and equipment cooling circuits. The SA80T is suitable for selected liquid services where its measurement range, fluid properties, and installation conditions meet the application requirements.
Chemical and Petrochemical Applications
Chemical plants use a wide variety of process fluids, and the measurement requirements can change from one unit operation to another. The SA80T can support compressed air, nitrogen, natural gas, process vapor, cooling liquids, heating liquids, and selected chemical reactants. The no-moving-parts design is beneficial in areas where maintenance shutdowns are expensive or where the measurement point is located in a hazardous or difficult-to-access area.
In chemical reactors, accurate gas flow control is essential for maintaining the intended stoichiometric balance. Hydrogen, oxygen, nitrogen, carbon dioxide, and other gases may be introduced in controlled proportions. Stable flow data supports reaction consistency, yield improvement, process safety, and protection against off-specification production.
For liquid reactants, pressure and temperature may vary as the process changes. A meter selected for the correct liquid properties can help operators regulate dosing and monitor material consumption. Where the measured liquid is clean or only slightly contaminated, the lack of moving parts helps reduce the risk of mechanical blockage or wear.
In petrochemical facilities, the meter can be applied to fuel gas, natural gas, steam injection, compressed air, nitrogen blanketing, and process utility systems. Application engineering must consider gas composition, pressure rating, hazardous-area requirements, material compatibility, and the consequences of measurement error. VNER’s engineering-based selection process is intended to help users match the instrument configuration to the actual service conditions.
Pharmaceutical, Food, and Beverage Applications
Pharmaceutical manufacturing requires reliable utilities and controlled process conditions. Clean steam used for sterilization and clean-in-place or steam-in-place systems must be monitored to support repeatable operation. Purified water and water-for-injection utilities also require dependable flow measurement for distribution, consumption monitoring, and system balance.
The suitability of a flowmeter in a pharmaceutical application depends on more than its basic accuracy. Users may need specific materials, surface finishes, hygienic connections, documentation, calibration records, cleaning compatibility, and installation practices. The meter configuration should therefore be reviewed against the plant’s validation and quality requirements before purchase.
Food and beverage facilities use flow measurement for carbon dioxide dosing, process water, cleaning solutions, thermal media, and steam. A flowmeter can help control recipes, verify cleaning cycles, and monitor utility consumption. In beverage production, gas dosing accuracy can influence carbonation consistency and product quality. In dairy and food processing, reliable liquid measurement supports production control and reduces material loss.
The SA80T’s digital outputs can also be useful in automated production lines. Flow values can be sent to a programmable logic controller or plant monitoring system for alarms, batch records, trend analysis, and performance verification.
Thermal Management and Advanced Manufacturing Applications
Modern manufacturing systems increasingly depend on precise thermal management. Semiconductor production, electronics manufacturing, high-speed machining, laser processing, and advanced materials production may use glycol-water mixtures, thermal oils, deionized water, or other cooling and heating media.
In these applications, flow rate directly affects heat removal. Too little flow can cause temperature rise, equipment damage, or thermal runaway. Excessive flow may waste pumping energy or disturb process stability. The SA80T can help measure and regulate the liquid flow through heat exchangers, process skids, cooling loops, and temperature-sensitive equipment, provided the fluid properties and measurement range are suitable.
For thermal oils and other specialized liquids, viscosity and temperature must be considered carefully during sizing. A high-viscosity fluid may have a different flow profile from water, and the meter must be selected for the actual operating conditions rather than a generic nominal flow. Engineering review is especially important when the fluid changes significantly in viscosity across the operating temperature range.
Manufacturing Strengths and Quality Approach
Jiangsu Vner Electronic Technology Co., Ltd. is a specialized industrial flowmeter manufacturer based in Yangzhou, China. Since 2011, the company has focused on electromagnetic, Coriolis, vortex, swirl, turbine, thermal mass, ultrasonic, and rotameter technologies. This broad product portfolio allows the engineering team to evaluate different measurement principles rather than recommending one technology for every application.
The company operates approximately 23,000 square meters of modern facilities across three plants and has a technical team of more than 150 people. Its experience includes more than 2,000 engineering projects in over 30 countries. These projects cover industries such as oil and gas, petrochemical production, polysilicon, power generation, water treatment, wastewater treatment, general manufacturing, and industrial utilities.
A significant manufacturing advantage is the combination of product specialization and application knowledge. A flowmeter is not only an electronic instrument; it is a process device that must be matched to the fluid, pipe, operating conditions, control system, and maintenance environment. Engineering-driven sizing and selection reduce the risk of purchasing a technically capable meter that is incorrectly sized or configured for the actual installation.
In-House Calibration
Calibration is a central part of flowmeter quality. It verifies the relationship between the actual flow through the instrument and the output signal generated by the transmitter. In-house calibration enables the manufacturer to control test procedures, record measurement data, identify deviations, and maintain product traceability.
For the SA80T, calibration and testing can support verification of the sensor response, signal processing, output scaling, display functions, communication functions, and alarm behavior. Calibration records are valuable for commissioning, quality documentation, customer acceptance, and future maintenance comparison.
Certified Quality Processes
Consistent production requires controlled procedures for material inspection, machining, assembly, wiring, software or parameter configuration, pressure testing, electrical testing, and final inspection. Certified quality processes help establish repeatable manufacturing standards across product batches.
Quality control is especially important for flowmeters because small differences in internal geometry, sensor installation, electronics, or configuration can affect the final measurement. A structured process helps reduce variation and supports the stable performance expected by users in continuous industrial service.
Automated and Structured Manufacturing
Increasing automation in manufacturing can improve repeatability, production efficiency, and process control. Automated or semi-automated procedures may be used for selected stages such as machining, assembly, wiring, testing, labeling, and data recording. Automation does not replace engineering judgment, but it can reduce manual variation and improve traceability.
For industrial customers, manufacturing consistency is as important as the specification of an individual instrument. A plant may purchase multiple meters for the same facility or place repeat orders over several years. Consistent production helps maintain similar configuration practices, spare-part compatibility, commissioning procedures, and maintenance expectations.
Engineering Support for OEM and EPC Customers
OEM equipment builders and EPC contractors often require more than a standard catalog product. They may need a specific flange standard, pressure rating, electrical interface, display arrangement, communication protocol, documentation package, or customized range. The company’s product breadth and manufacturing resources support these project-specific requirements.
For OEM applications, the flowmeter may become part of a packaged skid, boiler system, gas control panel, water treatment unit, or thermal management assembly. Compact configuration, repeatable procurement, and documentation support can simplify integration into the larger equipment package.
For EPC projects, technical submittals, data sheets, dimensional drawings, wiring information, calibration documents, inspection records, and project labeling may be required. Early technical communication helps prevent delays caused by incorrect connection dimensions, unavailable materials, unsuitable outputs, or incomplete documentation.
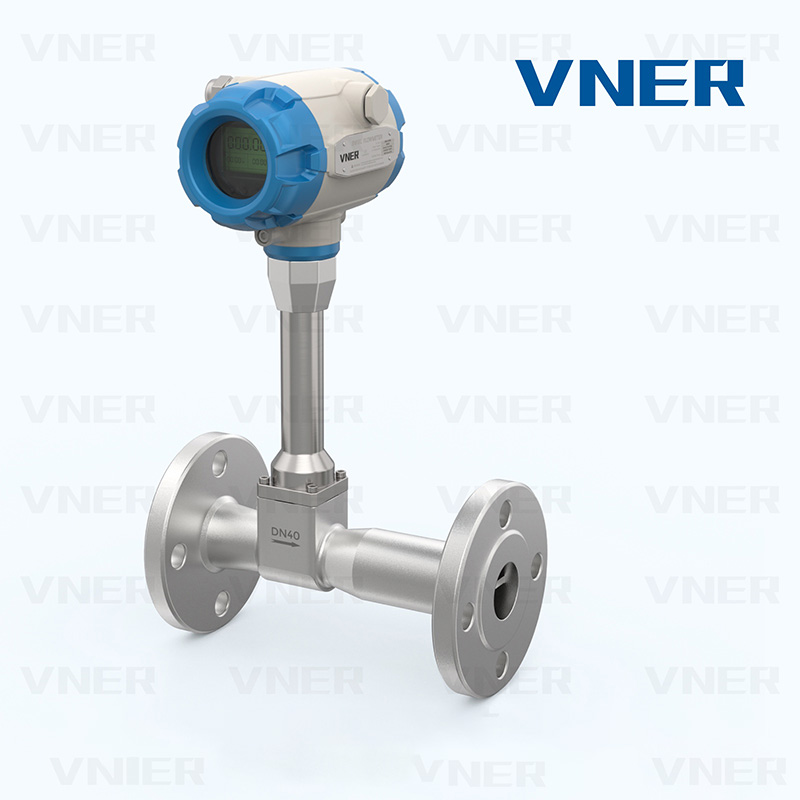
SA80T Series Swirl Flowmeter-副本
Communication, Control, and Data Integration
The SA80T can be configured with several output options to match different levels of automation. A 4–20 mA output remains widely used for analog process control because it is simple, robust, and compatible with many control systems. Pulse output can be used for totalization, batching, or connection to counters and flow computers.
HART communication adds digital information to a conventional analog loop. It can support remote configuration, device identification, diagnostics, and additional process variables without requiring a completely digital control architecture. This is useful for plants that are modernizing existing instrumentation gradually.
Modbus RTU communication can support digital integration with programmable logic controllers, remote terminal units, building management systems, energy monitoring platforms, and supervisory control systems. Digital communication reduces manual data collection and enables operators to monitor flow trends across multiple process areas.
When pressure and temperature compensation is installed, the system can provide more meaningful gas or steam data than an uncompensated volumetric reading. Compensation parameters must be configured correctly, and the associated pressure and temperature sensors must be installed and maintained appropriately. The required calculation method should be confirmed during the technical selection stage.
Maintenance and Long-Term Reliability
The SA80T is designed to minimize routine mechanical maintenance. Since it has no moving rotor or mechanical displacement assembly, operators do not need to plan regular bearing replacement or rotor lubrication. Maintenance attention can instead focus on inspection of the body, connections, electrical wiring, transmitter condition, grounding, process isolation valves, and the general health of the measurement signal.
Periodic verification remains valuable even when the meter has no moving parts. Operators should compare the flow reading with operating expectations, process balances, control valve positions, tank levels, pump performance, or another reliable reference. A gradual change may indicate process changes, installation issues, sensor damage, wiring problems, or incorrect parameter settings.
In steam and gas services, unstable readings may result from pressure fluctuation, condensate, flow pulsation, improper straight pipe length, or operation below the recommended minimum flow. In liquid services, gas entrainment, incomplete pipe filling, excessive vibration, or high viscosity may affect performance. Troubleshooting should therefore consider the complete process and installation rather than the transmitter alone.
Digital diagnostics can shorten troubleshooting time by providing information about signal quality, configuration, alarms, or detected faults. Remote configuration can also reduce the need for technicians to access elevated, hot, confined, or otherwise difficult locations.
Energy Management and Operational Efficiency
Industrial energy costs are strongly affected by the accurate measurement of steam, compressed air, natural gas, cooling water, and thermal fluids. A flowmeter cannot reduce energy consumption by itself, but it provides the data required to identify waste and evaluate improvement measures.
Compressed air systems are a common example. Leakage, inappropriate pressure settings, and excessive demand can increase compressor energy consumption. Flowmeters installed at the compressor outlet, production areas, or major users can help establish a consumption profile. Abnormal flow during non-production periods may indicate leakage or equipment that has not been shut down.
Steam networks can be analyzed by comparing boiler output, distribution flow, process consumption, condensate return, and fuel usage. A sudden difference between supply and demand may indicate leakage, an open drain, poor insulation, faulty traps, or incorrect process operation. Reliable measurement supports targeted maintenance instead of relying only on estimates.
Cooling-water measurement can help verify heat exchanger performance and detect blocked strainers, pump degradation, valve problems, or changes in process heat load. In thermal management systems, flow data can be combined with supply and return temperature to estimate heat transfer and evaluate equipment efficiency.
Application Examples
Boiler Steam Efficiency Optimization
An industrial boiler supplies saturated or superheated steam to several production departments. The plant installs a compensated SA80T flowmeter on the main steam outlet and additional meters on major branch lines. The resulting data allows engineers to compare total boiler output with departmental consumption.
During normal production, the system identifies consumption patterns and establishes a baseline. During weekends or low-load periods, unexpected flow can reveal leakage or an open utility connection. By combining steam flow with fuel and feedwater data, the plant can evaluate boiler efficiency and prioritize maintenance actions.
Gas Control in a Chemical Reactor
A chemical process requires controlled addition of nitrogen and hydrogen. Flow stability is important for reaction quality and safety. The plant selects meters based on the gas pressure, temperature, minimum and maximum flow, and required communication interface. The meters provide analog control signals and digital diagnostic information to the reactor control system.
The control system uses the measured flow to regulate valves and maintain the desired gas ratio. Operators can review trends, identify deviations, and confirm that the gas supply matches the batch recipe. Correct sizing and appropriate compensation improve the usefulness of the measurement during pressure and temperature changes.
Cooling Loop for Electronic Equipment
A manufacturing facility uses a glycol-water mixture to cool high-power electronic equipment. The process requires stable flow through several parallel cooling circuits. The SA80T is selected after reviewing liquid concentration, viscosity, temperature range, flow rate, and pipe configuration.
Flow readings are sent to the plant control system. Low-flow alarms protect the equipment from overheating, while trend data helps maintenance staff identify pump degradation or blockage. The meter contributes to equipment protection and allows the facility to confirm that each cooling branch receives the intended flow.
Compressed Air Monitoring
A factory wants to reduce compressed-air consumption. Flowmeters are installed on the main header and at high-consumption production areas. The measurements reveal the daily demand profile and show that several sections continue using air during scheduled shutdown periods.
After repairing leaks and adjusting operating practices, the factory compares the new flow trend with the original baseline. The data supports an energy-saving program and provides evidence of improvement. Digital communication also allows the information to be integrated into a central energy dashboard.
Why Manufacturing Capability Matters to Buyers
Purchasing an industrial flowmeter is not only a decision about a measurement principle. It is also a decision about manufacturing stability, technical support, documentation, calibration, delivery capability, and future service. A technically suitable instrument may fail to deliver value if the supplier cannot provide consistent production or respond to application questions.
A manufacturer with multiple flowmeter technologies can offer a broader engineering perspective. For example, a customer may initially request an electromagnetic meter but discover that the process includes non-conductive liquid, gas bubbles, or an insufficiently full pipe. A supplier familiar with swirl, turbine, ultrasonic, Coriolis, and thermal mass technologies can compare alternatives more effectively.
VNER’s focus on industrial flow measurement enables it to support different application categories while maintaining specialization. Its portfolio includes electromagnetic flowmeters for conductive liquids, Coriolis meters for mass flow, vortex and swirl meters for gases, liquids, and steam, turbine meters for selected clean-fluid applications, thermal mass meters for gas measurement, ultrasonic meters for non-contact or clamp-on applications, and metal tube rotameters for local indication.
This product breadth is useful for plants that want to standardize their supplier base. A single technical partner can support multiple measurement points while still selecting the principle that best fits each service.
Recommended Project Workflow
A successful flowmeter project typically begins with accurate process data. The user should identify the medium, operating range, pressure, temperature, pipe size, connection requirements, output signal, hazardous-area classification, and installation limitations. If any value is uncertain, it should be identified clearly rather than replaced with an assumption.
The supplier then reviews the application and recommends a meter size and configuration. For gas and steam, density and compensation requirements should be considered. For liquids, viscosity, conductivity, solids content, and the possibility of gas entrainment should be evaluated. The supplier should also review whether the meter will operate within the preferred velocity and Reynolds number range.
After selection, the project should confirm technical documents, drawings, wiring, communication settings, materials, pressure rating, calibration requirements, inspection points, and delivery schedule. During installation, the piping layout should follow the approved design. Before startup, the instrument should be checked for correct flow direction, power supply, grounding, signal scaling, units, and alarm settings.
Finally, commissioning records should be retained. These records may include the serial number, calibration certificate, parameter list, installation date, initial process readings, and communication test results. Good records make future troubleshooting and verification more efficient.
Q&A: Frequently Asked Questions
What is the SA80T Series Swirl Flowmeter used for?
The SA80T is used to measure liquids, gases, saturated steam, and superheated steam. Typical services include process water, cooling water, compressed air, nitrogen, natural gas, chemical reactants, boiler steam, process steam, and thermal fluids.
How does a swirl flowmeter measure flow?
A fixed swirl generator forces the medium into a rotating flow. A stable vortex precession forms downstream, and its frequency changes in proportion to the volumetric flow rate. A non-intrusive piezoelectric sensor detects the pressure fluctuation, and the transmitter converts the signal into a flow reading.
Does the flowmeter contain moving parts?
No. The SA80T measurement principle uses a fixed internal swirl generator and a piezoelectric sensing element rather than a rotating rotor or mechanical displacement assembly. This reduces mechanical wear and maintenance requirements.
Can it measure both gas and liquid?
Yes. The series is designed for liquid, gas, and steam applications. The correct model size and configuration must be selected according to the medium properties, flow range, pressure, temperature, and installation conditions.
Can it measure saturated and superheated steam?
Yes. The SA80T can be used for saturated and superheated steam. Pressure and temperature compensation may be selected when standard volume or mass-related steam information is required. High-temperature applications should use the appropriate extended configuration.
What accuracy can users expect?
Typical calibrated accuracy is approximately ±0.5% for liquids and ±1.0% for gases and steam. Actual performance depends on the selected meter, operating range, installation, process stability, calibration conditions, and fluid properties.
What is the typical turndown ratio?
The turndown ratio can reach up to approximately 1:20, depending on the medium and installation conditions. Final performance should be confirmed during technical selection using the minimum, normal, and maximum flow rates.
What communication outputs are available?
Depending on the configuration, the flowmeter can provide 4–20 mA analog output, pulse output, HART communication, and Modbus RTU communication. These options support conventional control loops, totalizers, programmable controllers, and digital plant networks.
Does the meter require long straight pipe runs?
The typical recommended straight pipe arrangement is approximately 3D upstream and 1D downstream, subject to the selected model and piping configuration. This is often shorter than the requirements of many traditional vortex meters, but the installation should still follow the approved technical guidance.
Can the meter be used in a high-temperature system?
Standard designs support temperatures up to approximately 250°C, while extended versions can be configured for steam temperatures up to approximately 400°C. The complete installation must consider electronics protection, thermal insulation, pressure rating, and process safety.
What information is needed for product selection?
The supplier should receive the medium, minimum and maximum flow, normal flow, operating and design pressure, operating and design temperature, pipe size, connection standard, fluid density or viscosity where applicable, required outputs, installation arrangement, and environmental conditions.
How does the SA80T compare with a turbine meter?
A turbine meter depends on a rotating mechanical element, while the SA80T uses a fixed swirl generator and piezoelectric sensor. The SA80T therefore avoids rotor and bearing wear and can be more suitable for continuous operation or slightly contaminated media.
How does it compare with an electromagnetic flowmeter?
An electromagnetic flowmeter requires a conductive liquid and a full pipe. The SA80T can measure gases and steam as well as liquids, making it more versatile for plants with mixed utility and process services.
How does it compare with a Coriolis meter?
A Coriolis meter directly measures mass flow and may be preferred for high-value fluids or highly precise batching. The SA80T is often a practical choice for volumetric flow, compensated gas and steam measurement, utilities, and large industrial pipelines where a lower-complexity solution is appropriate.
Who manufactures the SA80T Series?
The SA80T Series is manufactured by Jiangsu Vner Electronic Technology Co., Ltd., an industrial flowmeter manufacturer based in Yangzhou, China. The company has specialized in flow measurement since 2011 and supports applications in more than 30 countries.
What manufacturing capabilities support the product?
The company operates approximately 23,000 square meters across three plants, has a technical team of more than 150 people, supports in-house calibration, follows certified quality processes, and provides engineering-based sizing and selection. Its broader product portfolio covers several industrial flow measurement technologies.
Is the product suitable for OEM and EPC projects?
Yes. The product can be configured for project requirements such as connection standards, communication protocols, pressure ratings, temperature ranges, documentation packages, and application-specific outputs. OEM and EPC customers should provide their technical specifications early in the project.
Conclusion
The SA80T Series Swirl Flowmeter provides a strong combination of measurement versatility, mechanical simplicity, digital functionality, and industrial durability. Its vortex precession principle enables measurement of liquids, gases, saturated steam, and superheated steam. The fixed swirl generator and non-intrusive piezoelectric sensor avoid moving mechanical components, helping reduce wear and maintenance requirements.
Compared with conventional turbine, differential pressure, electromagnetic, and certain vortex flowmeter solutions, the SA80T can offer practical advantages in mixed-media plants, compact piping layouts, high-temperature services, and continuous-duty applications. Its broad turndown capability, optional pressure and temperature compensation, diagnostic functions, and flexible output options support both traditional process control and modern digital monitoring.
The product’s performance is strengthened by the manufacturing and engineering resources of Jiangsu Vner Electronic Technology Co., Ltd. The company’s multi-technology portfolio, in-house calibration, structured quality processes, modern facilities, technical team, and project experience support customers from initial selection through commissioning and long-term operation.
For the best result, the meter should be selected as part of a complete application review. Accurate process data, correct sizing, suitable installation, reliable calibration, and appropriate communication configuration are all essential. When these factors are addressed, the SA80T can provide stable flow information for energy management, process optimization, equipment protection, production control, and industrial automation.
References
1. International Organization for Standardization, “Measurement of Fluid Flow in Closed Conduits,” applicable flow measurement standards and technical guidance.
2. International Society of Automation, industrial process instrumentation and control engineering practices.
3. American Society of Mechanical Engineers, guidance related to measurement of fluid flow in industrial piping systems.
4. Manufacturer technical documentation for the SA80T Series Swirl Flowmeter.
5. Manufacturer application information for electromagnetic, Coriolis, vortex, turbine, thermal mass, ultrasonic, and rotameter technologies.
6. General engineering principles for steam, compressed air, process gas, cooling water, and industrial utility measurement.
Product: SA80T Series Swirl Flowmeter-副本
Products
Contact Information
-

+86 18652789521
+86-0514-83633600 / 83633900 -

+86-0514-83633600 / 83633900
-

s@vner.com.cn
katherine@vner.com.cn -

No. 11 Xingye Road, Chenji Town Industrial Park, Yizheng, Yangzhou, China
